
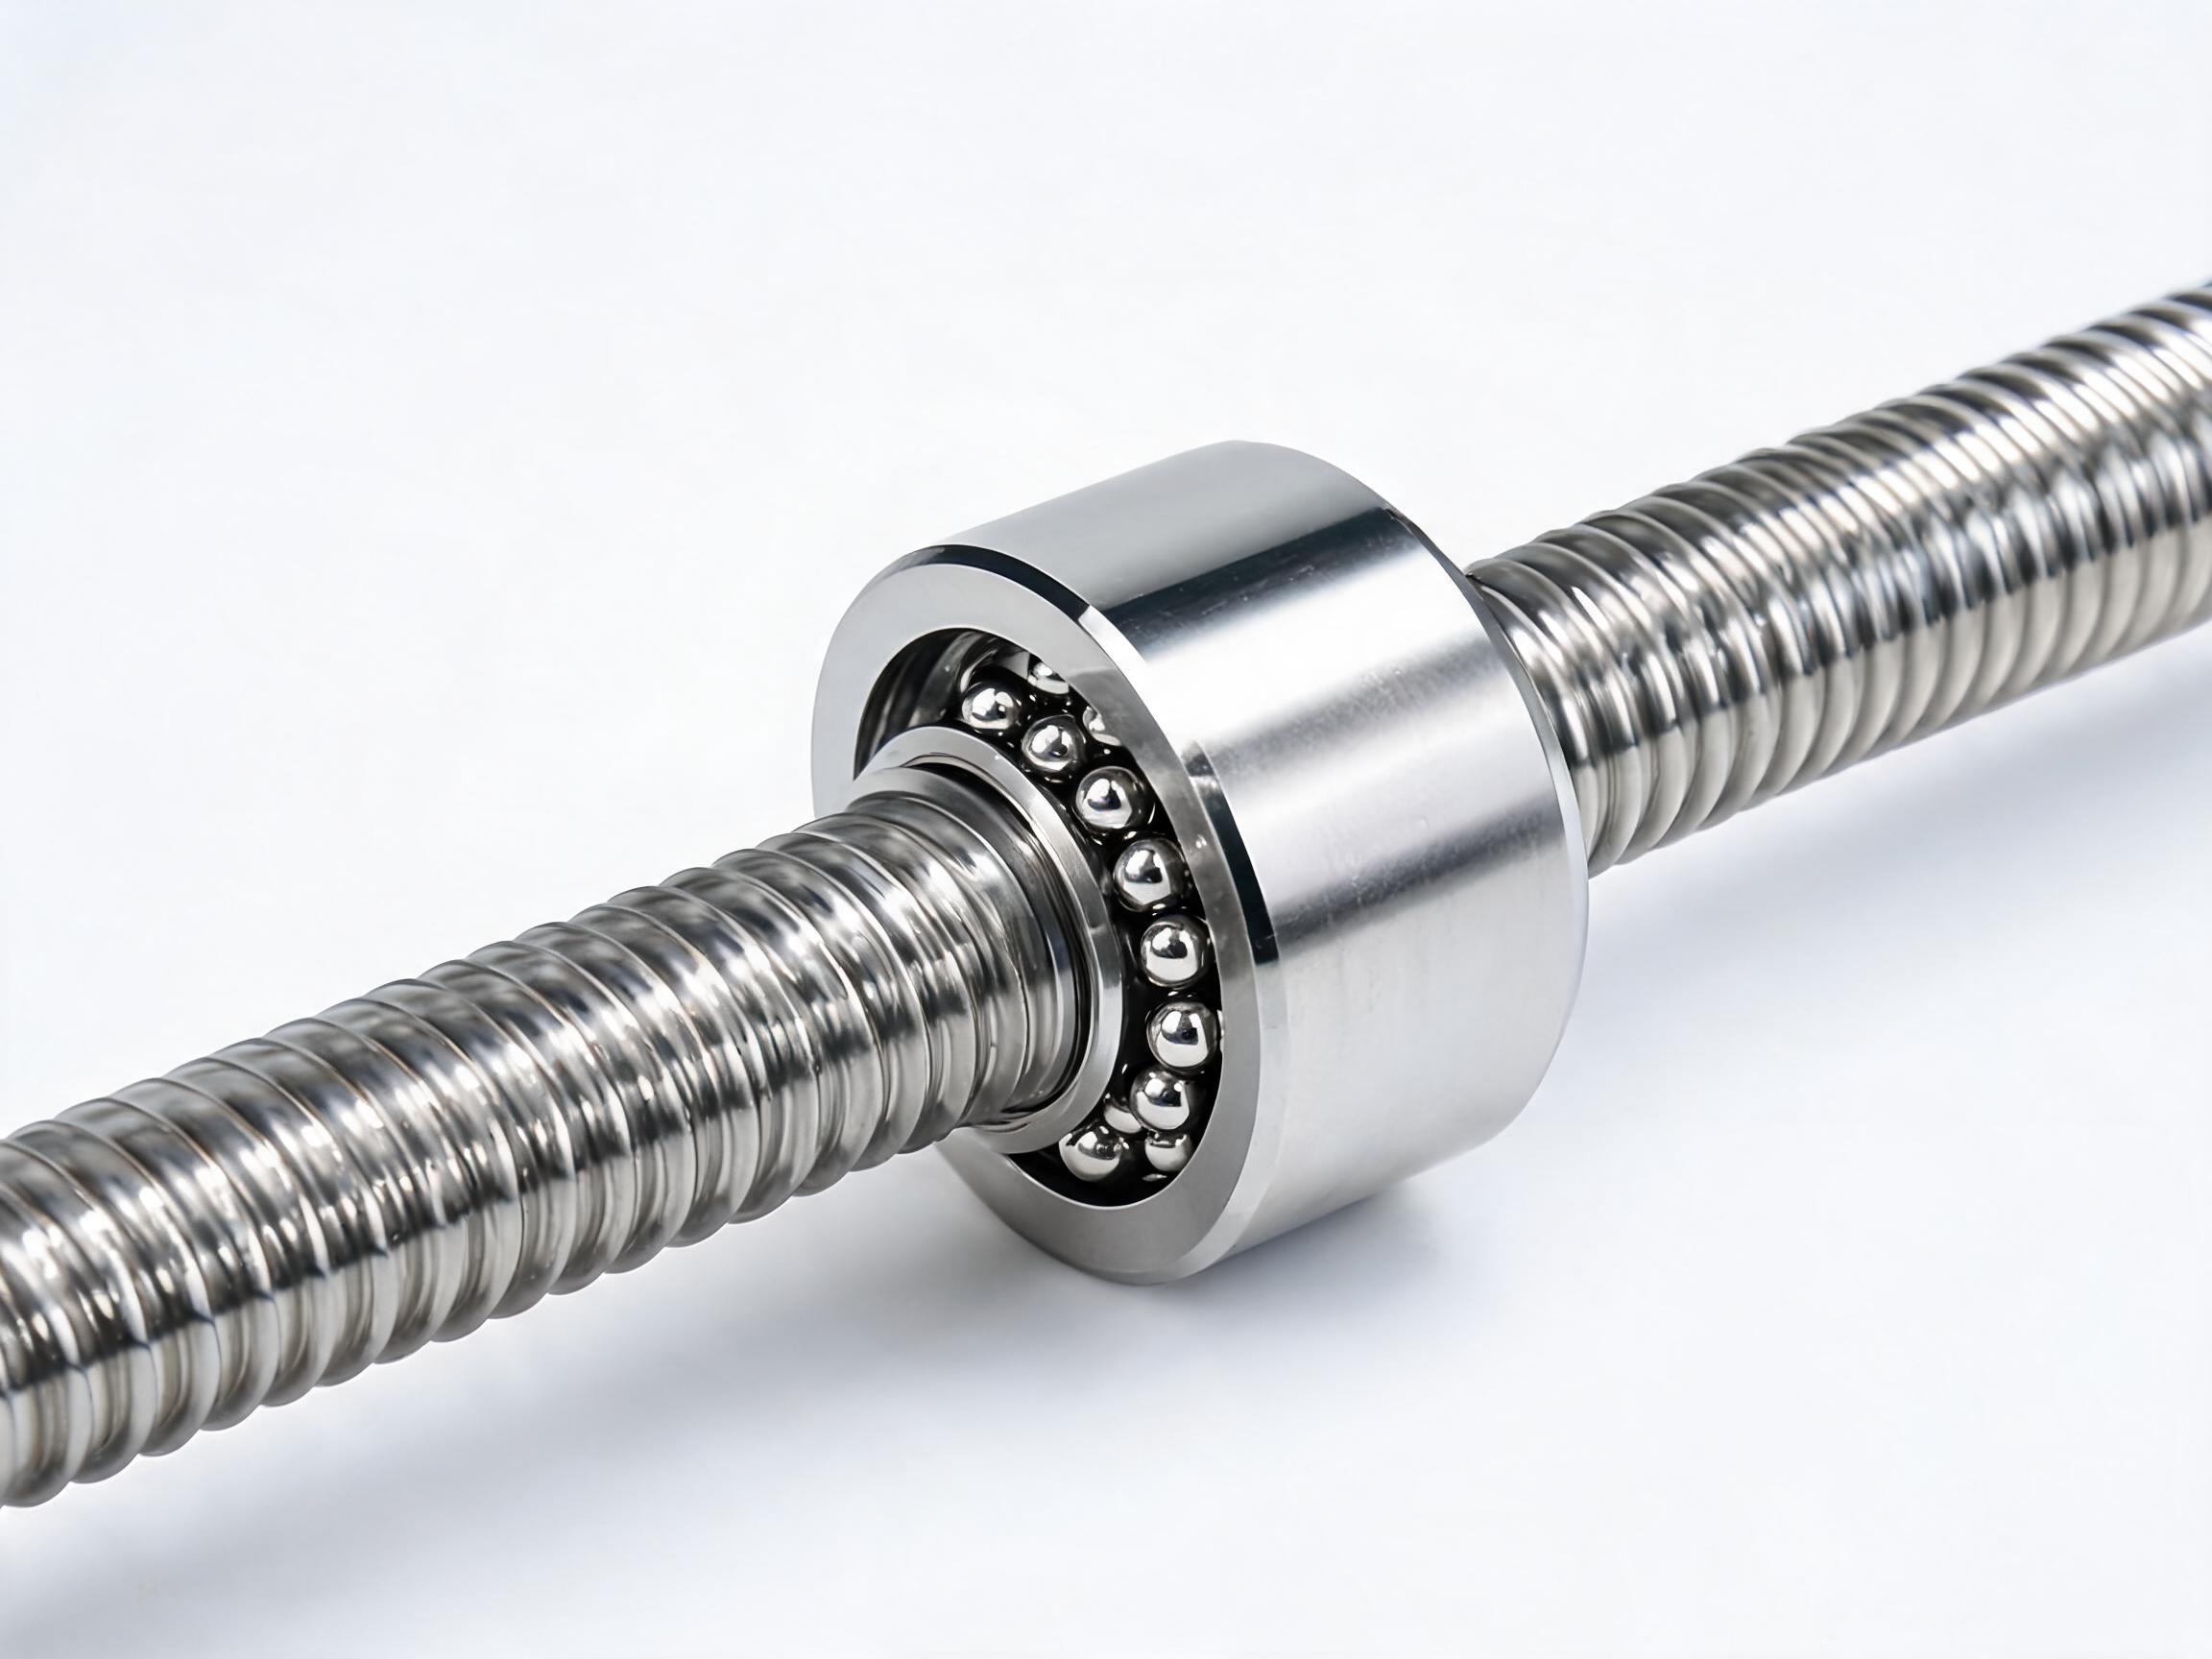
A practical guide for procurement engineers and buyers. This article breaks down the four critical decisions in ball screw selection—manufacturing process (rolled vs. ground), precision grade (C3/C5/C7), preload method, and application matching—with comparison tables and actionable criteria. Written for international buyers who need to specify the right component without overpaying for unnecessary precision.
BALL SCREW BUYER GUIDE
Ball Screw Selection Guide: Rolled vs. Ground, Precision Classes, Preload Methods, and Application Matching
Selecting the right ball screw is not about picking the most expensive option—it is about matching the component to the machine's actual performance requirements. A CNC lathe that needs 0.005 mm positioning accuracy does not require the same screw as a packaging machine that runs at 0.1 mm repeatability. Specifying the wrong grade wastes money; specifying the wrong manufacturing process can cause premature failure.
This guide covers the four decisions every buyer must make when sourcing a ball screw: rolled vs. ground manufacturing, precision class selection, preload method, and application matching. Each section includes concrete criteria you can use in your RFQ.
- Rolled screws cover roughly 80% of industrial applications at 30–50% lower cost than ground screws—start here unless your application demands otherwise.
- Precision class (C3/C5/C7) must be matched to the machine's actual positioning requirement, not the marketing brochure's claim.
- Preload eliminates backlash but adds heat and reduces efficiency—over-preloading is a common design error.
- Application matching means considering speed, load direction, duty cycle, and environmental factors before finalizing a spec.
1. Rolled vs. Ground: The First Decision
The manufacturing process determines the screw's accuracy ceiling, surface finish, and cost. There is no "better" option—only the right option for your application.
Rolled Ball Screws
Rolled ball screws are produced by thread rolling, a cold-forming process that displaces material rather than cutting it. The thread profile is formed by rolling dies that press the blank into shape.
Typical specifications:
- Lead accuracy: 50–100 µm per 300 mm (C7–C10 class)
- Surface finish: Good, but with a work-hardened layer
- Production cost: Low—suitable for volume manufacturing
- Lead time: Short, typically 2–4 weeks for standard sizes
Best applications:
- General automation and material handling
- Packaging machinery
- Welding and cutting tables
- Low-to-medium precision CNC machines (drilling, tapping)
- Any application where cost per unit matters more than sub-micron accuracy
Ground Ball Screws
Ground ball screws start as rolled blanks, then the thread profile is precision-ground after heat treatment. This removes the hardened layer, corrects lead errors, and produces a smoother, more accurate thread surface.
Typical specifications:
- Lead accuracy: 5–25 µm per 300 mm (C1–C5 class)
- Surface finish: Superior—lower friction and less wear
- Production cost: 2–3× higher than rolled
- Lead time: Longer, typically 6–10 weeks
Best applications:
- CNC machining centers and lathes
- Precision positioning stages (semiconductor, PCB drilling)
- EDM machines, grinders, and measuring equipment
- Applications requiring high stiffness and minimal thermal drift
| Comparison Criteria | Rolled | Ground |
|---|---|---|
| Lead accuracy (per 300mm) | 50–100 µm (C7–C10) | 5–25 µm (C1–C5) |
| Relative cost | 1× (baseline) | 2–3× |
| Surface hardness | Work-hardened layer | Removed by grinding |
| Typical lead time | 2–4 weeks | 6–10 weeks |
| Noise level | Higher | Lower |
| Typical applications | Automation, packaging, general machinery | CNC, precision positioning, measuring |
Rule of thumb: If your positioning tolerance is above ±0.02 mm, a rolled screw with C7 accuracy will likely meet your needs at a fraction of the cost. Only move to ground when the application genuinely requires it.
2. Precision Classes: What C3, C5, and C7 Actually Mean
Precision class is defined by the maximum allowable lead error over a specified travel length. The JIS B1192 standard is the most commonly referenced specification in international trade.
The Standard Classes
| Class | Lead Error (µm/300mm) | Typical Applications | Relative Cost |
|---|---|---|---|
| C1 | 5 | Ultra-precision measuring, semiconductor | 4–5× |
| C3 | 8 | High-end CNC, precision grinding | 3–4× |
| C5 | 18 | Standard CNC, precision automation | 2–3× |
| C7 | 50 | General automation, packaging | 1× |
| C10 | 100+ | Positioning with feedback compensation | 0.8× |
How to Choose the Right Class
The precision class should be selected based on the machine's positioning accuracy requirement, not the encoder resolution or the servo motor's rated precision.
A practical selection method:
- Determine the machine's required positioning accuracy (e.g., ±0.01 mm)
- Account for other error sources: thermal expansion, servo following error, mechanical backlash (typically 30–50% of total error budget)
- The ball screw's lead error should be no more than 50% of the remaining error budget
- Select the class that meets this calculated requirement
Example: A machine needs ±0.03 mm positioning accuracy. Thermal and servo errors consume about 0.015 mm. The remaining budget for the screw is 0.015 mm. A C5 screw (18 µm/300mm) fits this budget; C7 (50 µm) does not.
3. Preload Methods: Eliminating Backlash
Backlash—the clearance between the ball and the thread groove—causes positioning error when the direction of travel reverses. Preload removes this clearance by applying an internal force that keeps the balls in contact with both flanks of the thread.
Preload Methods Compared
Single-Nut with Oversized Balls
- How it works: Balls are selected slightly larger than the nominal size to create interference
- Preload ratio: 2–5% of dynamic load
- Pros: Simple, compact, low cost
- Cons: Limited preload range, wear reduces preload over time
- Best for: Light-to-medium loads, general automation
Double-Nut with Shim
- How it works: Two nuts are separated by a shim of precise thickness; the shim pushes the nuts apart, creating preload
- Preload ratio: 5–10% of dynamic load
- Pros: High and consistent preload, adjustable
- Cons: Longer assembly, requires precise shim selection
- Best for: CNC machines, applications requiring high stiffness
Double-Nut with Spring
- How it works: A spring between two nuts provides constant preload force
- Preload ratio: 1–3% of dynamic load
- Pros: Constant preload regardless of wear, forgiving of thermal expansion
- Cons: Lower stiffness, not suitable for heavy cutting
- Best for: Light precision positioning, vertical axes
Double-Nut with Threaded Adjuster
- How it works: One nut is threaded; rotation adjusts the distance between nuts
- Preload ratio: Adjustable up to 10%+ of dynamic load
- Pros: Field-adjustable, highest stiffness
- Cons: Most expensive, requires skilled adjustment
- Best for: High-end CNC, precision grinding machines
| Preload Method | Stiffness | Cost | Adjustability | Typical Use |
|---|---|---|---|---|
| Oversized balls (single nut) | Low–Medium | Low | None | General automation |
| Shim (double nut) | High | Medium | By shim change | CNC, machining |
| Spring (double nut) | Low | Medium | Self-adjusting | Light positioning |
| Threaded adjuster | Highest | High | Field-adjustable | High-end precision |
Preload and Heat: The Trade-Off
Higher preload increases stiffness but also increases friction and heat generation. Excessive heat causes thermal expansion, which can reduce accuracy—defeating the purpose of the preload.
Selection guidance:
- Light preload (2–3%): For high-speed applications where heat is a concern
- Medium preload (5–7%): For general CNC machining—balanced stiffness and heat
- Heavy preload (8–10%): Only for low-speed, high-stiffness applications like grinding
4. Application Matching: Putting It All Together
The final step is matching the complete screw specification to the machine's operating conditions. Four factors matter most: speed, load, duty cycle, and environment.
Speed Considerations
- Critical speed: Every ball screw has a maximum rotational speed determined by its length, diameter, and support method. Exceeding this causes whipping (resonance).
- DN value: The product of screw diameter (mm) and rotational speed (rpm). For standard ball screws, DN ≤ 70,000–100,000. For high-speed designs, 120,000–150,000 is possible with special ball return systems.
- Lead selection: Higher lead means higher linear speed at the same RPM, but also lower resolution. Match the lead to the required feed rate and the motor's rated speed range.
Load and Life Calculation
The basic dynamic load rating (Ca) and the applied axial load determine the screw's L10 life:
- L10 life (hours) = (Ca / Fa)³ × 10⁶ / (60 × n)
- Where Fa = equivalent axial load (N), n = rotational speed (rpm)
Practical guidance:
- For continuous operation, target an L10 life of at least 20,000 hours
- For intermittent duty, 10,000–15,000 hours is often acceptable
- Consider both axial and radial loads—misalignment reduces life significantly
Environmental Factors
- Contamination: Ball screws are sensitive to dust and chips. Specify wipers (scrapers) for dirty environments.
- Lubrication: Grease for standard applications (relubrication interval 3–6 months), oil for high-speed applications. Food-grade lubricants for food processing machinery.
- Temperature: Standard ball screws operate from -20°C to +80°C. For higher temperatures, special materials and clearances are required—consult the manufacturer.
Vertical vs. Horizontal Mounting
Vertical axes require special consideration:
- Preload is mandatory to prevent the nut from dropping under gravity when the motor is off
- Spring preload is often preferred because it maintains constant force as the screw wears
- Brake or counterweight may be needed for safety in case of power loss
5. Common Selection Errors to Avoid
Error 1: Over-specifying precision. A C3 screw on a packaging machine is wasted money. The machine's other components (linear guides, couplings, structure) cannot deliver the accuracy the screw is capable of.
Error 2: Ignoring thermal effects. High preload + high speed = heat = expansion = lost accuracy. Calculate the expected temperature rise and its effect on lead error.
Error 3: Mismatching lead and motor. A servo motor at 3000 rpm with a 10 mm lead gives 30 m/min linear speed. If your machine only needs 10 m/min, a 5 mm lead would give better resolution and lower inertia mismatch.
Error 4: Forgetting the nut's moment load. In many applications, the nut is subjected to a tilting moment (e.g., cantilevered loads). This reduces life and can cause jamming. Specify a nut with sufficient flange size and check the moment load rating.
Error 5: Not specifying the end machining. Ball screws are typically supplied with unmachined ends. The buyer must specify shaft end machining (diameter, length, keyways, threads) to match the bearing and coupling. This is a common source of delays—provide a detailed shaft end drawing with your RFQ.
6. What to Include in Your RFQ
A complete ball screw RFQ should include:
- Screw diameter and lead (e.g., 25 mm diameter, 10 mm lead)
- Overall length and thread length (with a drawing if possible)
- Precision class (C5, C7, etc.)
- Preload method and preload amount (if required)
- Nut type (flanged, cylindrical, or custom)
- Shaft end machining (drawing or detailed dimensions)
- Operating conditions (speed, load, duty cycle, temperature)
- Mounting orientation (horizontal or vertical)
- Lubrication requirement (grease type, food-grade, etc.)
- Quantity and target lead time
FAQ
Q: Can a rolled ball screw achieve C5 precision? A: Yes. Some manufacturers offer rolled screws with C5 accuracy by using precision rolling dies and selective assembly. However, the consistency and surface finish may not match ground screws at the same class. For critical applications, ground is safer.
Q: How do I know if I need preload? A: If your application involves frequent direction reversals and requires consistent positioning accuracy, preload is necessary. For continuous one-direction motion (e.g., a feed axis that always moves the same way), backlash may be acceptable.
Q: What is the typical lead time for custom ball screws? A: Standard sizes with rolled threads: 2–4 weeks. Ground screws: 6–10 weeks. Custom shaft end machining adds 1–2 weeks. Always confirm lead time with the supplier before placing an order.
Q: Can I replace a ground screw with a rolled one in an existing machine? A: Only if the machine's positioning requirements are within the rolled screw's accuracy. Check the original screw's precision class and compare. Also verify that the nut dimensions and shaft ends are compatible—rolled screws often have different nut profiles.
Q: How should I handle lubrication for a ball screw in a dusty environment? A: Use lithium-based grease with a relubrication interval of 3–6 months, and ensure the screw is equipped with wipers on both ends of the nut. For heavy dust, consider a protective bellows cover.
Need help specifying the right ball screw for your application? Send us your machine's operating parameters—speed, load, accuracy requirement, and mounting orientation—and we will recommend the appropriate screw type, precision class, and preload method. Contact our engineering team for a detailed quotation.