
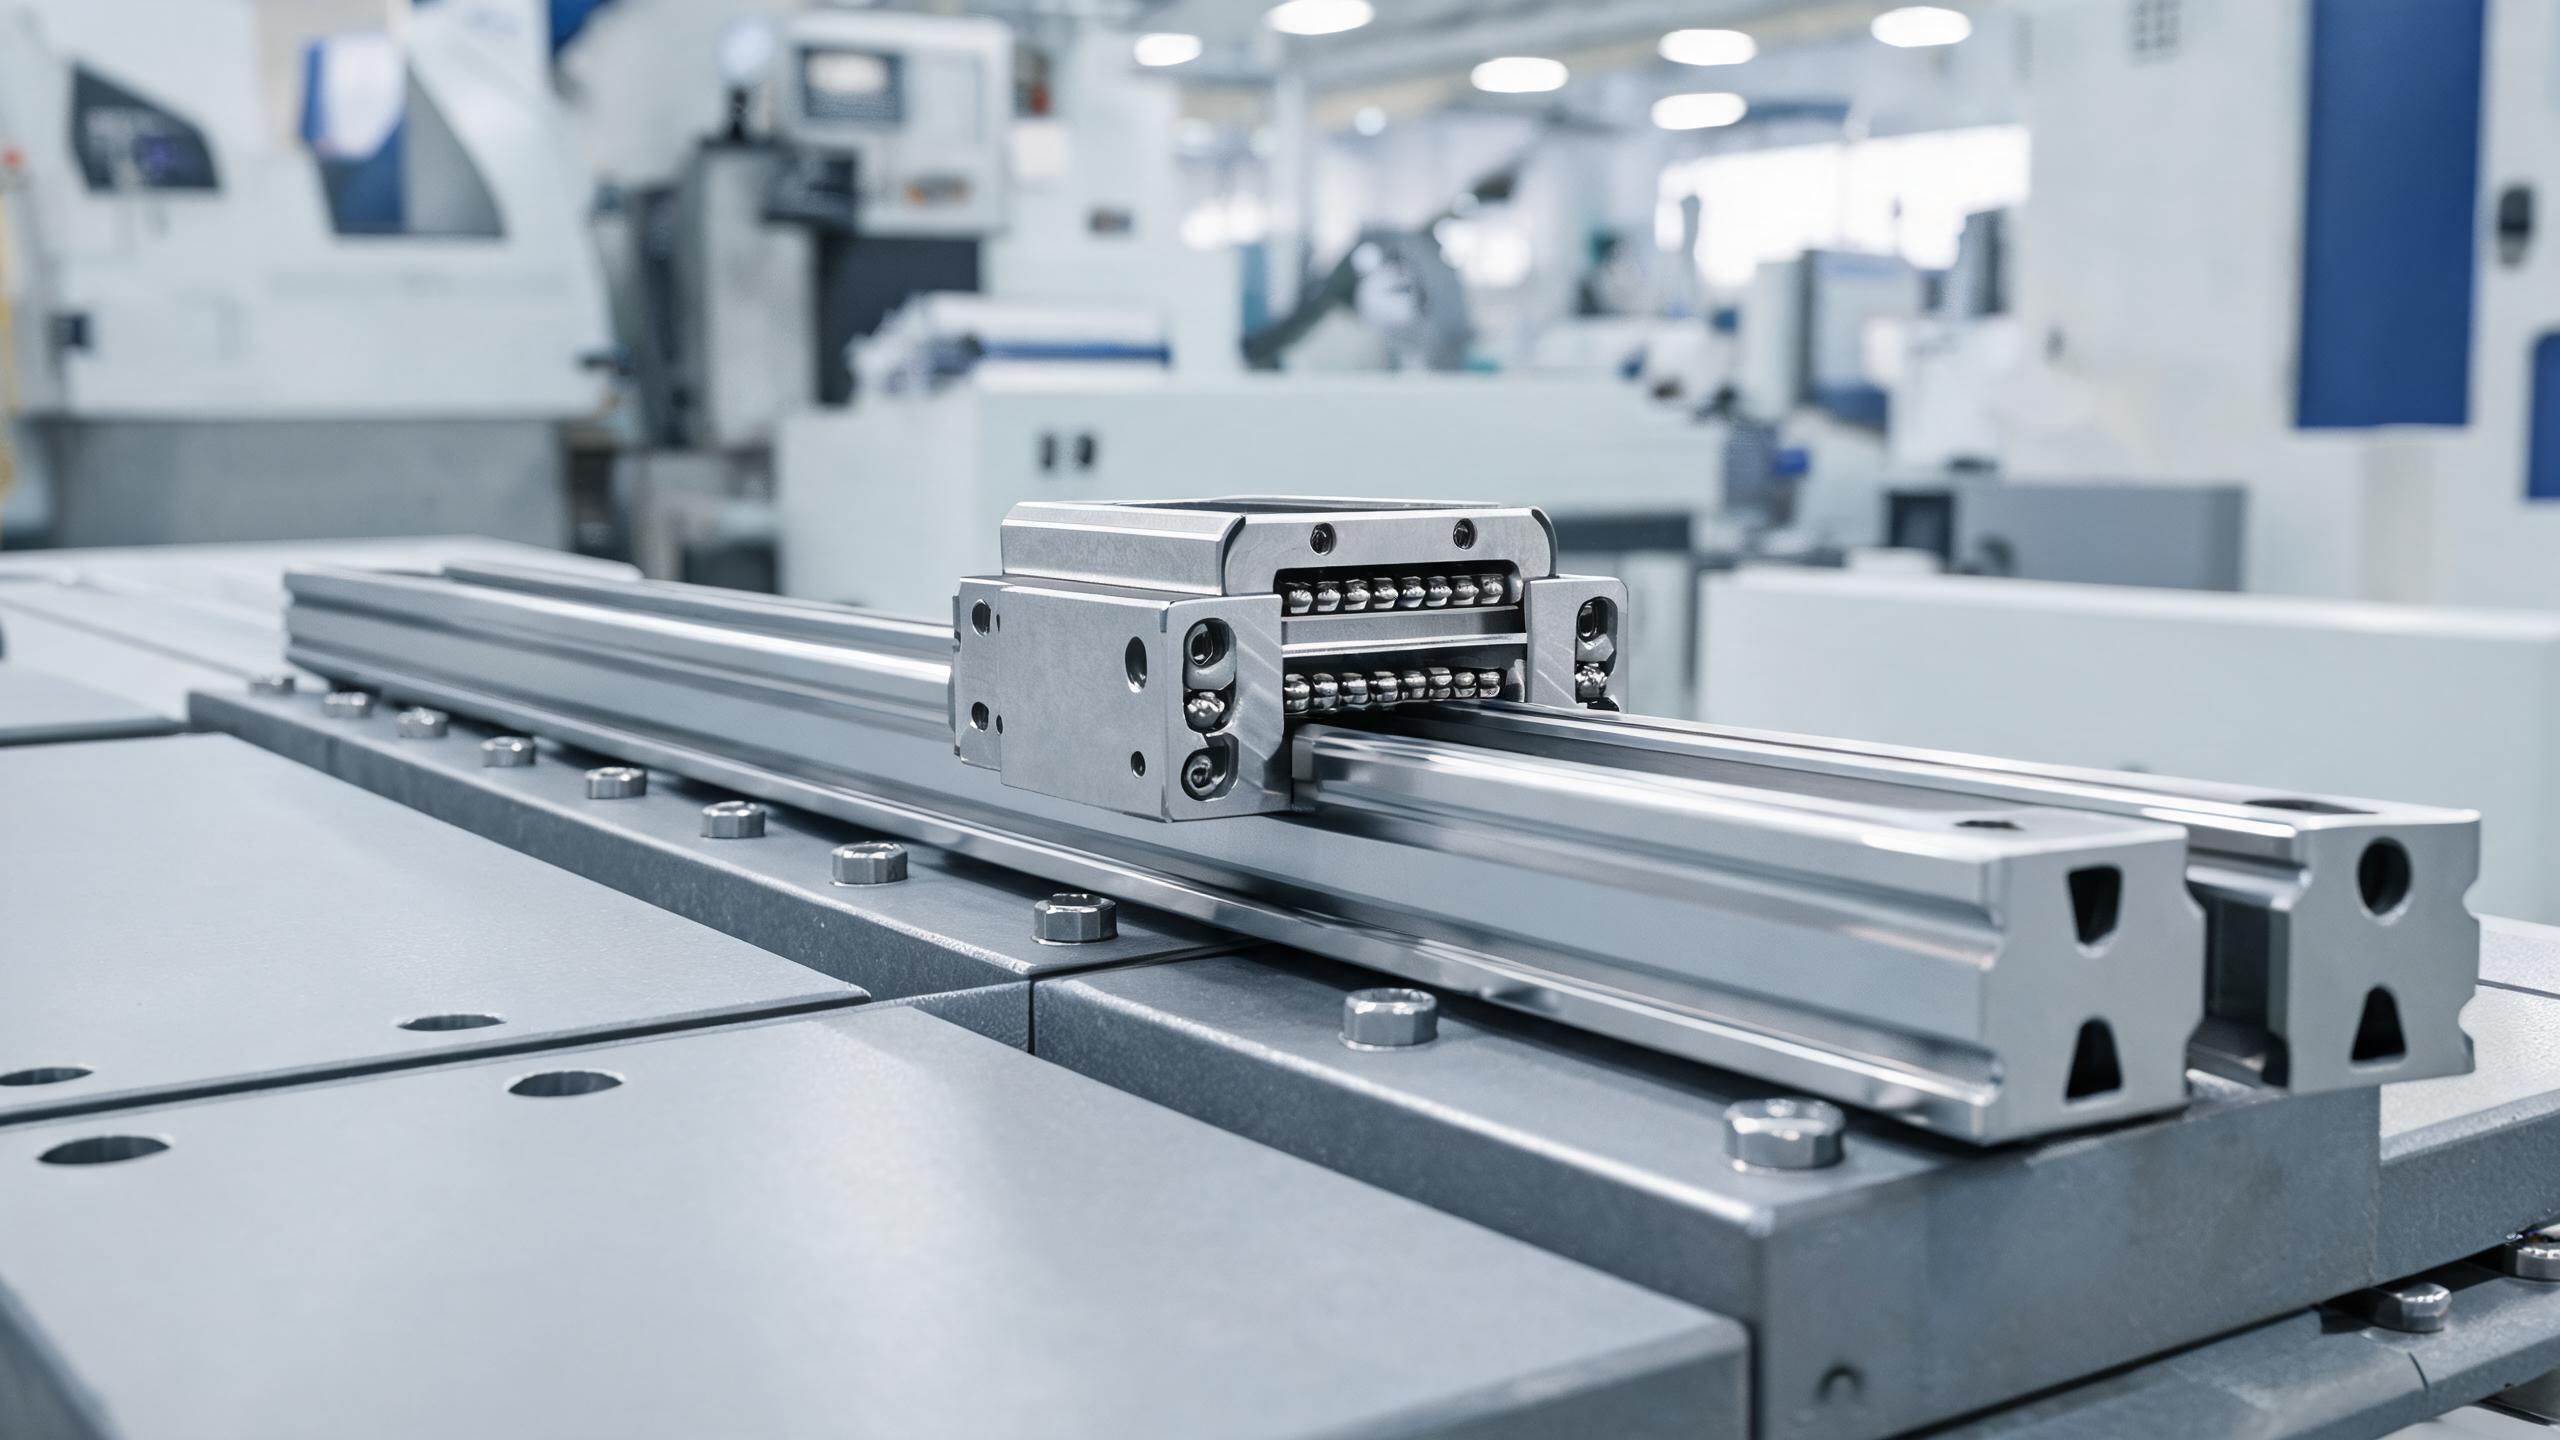
A practical buyer's guide to selecting linear carriages (linear guide bearing blocks) for B2B motion-control applications. Covers load rating math, preload class trade-offs, mounting and accuracy grades, sealing, and supplier evaluation — written for procurement engineers who need to spec the right linear bearing block the first time.
BUYER GUIDE — LINEAR MOTION COMPONENTS
If you are sourcing a linear carriage for a new machine or replacing one in an existing guideway system, the datasheet gives you more numbers than you can act on. Dynamic load, static load, preload class, accuracy grade, rail width, block height — each parameter changes the cost and the working life of the assembly.
This guide is written for procurement engineers and machine builders who need to make a defensible selection. We cover the three decisions that matter most — load rating math, preload class, and mounting/accuracy options — and we end with a supplier checklist so you can compare quotes on the same basis.
- Size the carriage by dynamic load rating (C) against the actual load spectrum, then verify static safety factor at peak load.
- Preload class is a stiffness-vs-life trade-off: light preload (Z0/ZF) for general use, medium (Z1) for CNC, heavy (Z2/Z3) only for rigid, low-duty applications.
- Accuracy grade (C0–C5) and mounting surface finish determine real-world performance more than the block itself.
- Ask suppliers for certified dimensional reports and material certificates — not just a catalog page.
Why the Linear Carriage Selection Matters
The linear carriage — also called a linear guide bearing block or linear bearing block — is the moving interface between the rail and the machine table. It carries the load, transmits the drive force, and determines the positioning repeatability of the axis.
An undersized carriage fails early. An oversized one adds cost and inertia, which reduces acceleration and increases motor torque requirements. The goal is a carriage that runs at 15–25% of its dynamic load rating under normal operation — that is the sweet spot for service life and cost.
1. Load Ratings: The Math That Determines Life
Every linear guide bearing block datasheet lists two load numbers:
- Dynamic load rating (C) — the load at which 90% of a population of identical blocks will achieve a rated travel of 50 km (per ISO 14728-1).
- Static load rating (C0) — the load at which permanent deformation of the rolling elements or raceways begins.
Service life is calculated with the basic rating life formula:
L = (C / P)³ × 50 km
Where P is the equivalent dynamic load (the combined radial and moment loads, calculated per the manufacturer's method). The cubic exponent means small changes in load produce large changes in life. Double the load — life drops to one-eighth.
How to Apply Load Ratings in Practice
Most applications do not run at a single constant load. The correct approach is to build a load spectrum:
- List each phase of the machine cycle (acceleration, steady feed, cutting, deceleration, dwell).
- Calculate the load on each carriage block for each phase.
- Compute the equivalent dynamic load P using the manufacturer's formula.
- Check the static safety factor: C0 / P_peak ≥ 2 for normal operation, ≥ 3–5 for shock loads or high-vibration machines.
| Application Type | Recommended Static Safety Factor (fs) | Typical Duty |
|---|---|---|
| General automation, assembly | 2.0 – 3.0 | Light, intermittent |
| CNC machine tools, machining centers | 3.0 – 5.0 | Medium, continuous with cutting forces |
| Heavy-duty presses, stamping, forging | 5.0 – 7.0 | High shock loads |
| High-speed pick-and-place, packaging | 2.5 – 3.5 | High acceleration, low load per cycle |
If the supplier cannot provide the equivalent-load calculation method, treat that as a red flag. A reputable manufacturer will publish the full calculation procedure in their technical catalog.
2. Preload Classes: Stiffness vs. Life
Preload is the internal force applied between the balls or rollers and the raceways, set at the factory by using slightly oversized balls or by the geometry of the block. It eliminates internal clearance, which improves rigidity and positioning accuracy — but it also increases friction and running temperature, which reduces service life.
Preload classes are typically designated as follows (the exact symbols vary by manufacturer, but the logic is consistent):
| Preload Class | Clearance / Interference | Typical Applications | Trade-off |
|---|---|---|---|
| Z0 / Clearance (C) | Small positive clearance | Single-axis handling, low precision | Lowest friction, longest life, some play |
| Z1 / Light preload (P0) | Light interference | General automation, assembly lines, packaging | Balanced stiffness and life — most common choice |
| Z2 / Medium preload (P1) | Medium interference | CNC routers, milling, grinding, high-precision positioning | High stiffness, moderate life reduction |
| Z3 / Heavy preload (P2) | Heavy interference | Heavy cutting, high-rigidity machine tools | Maximum stiffness, shortest life, higher drive torque |
How to Choose the Right Preload Class
The rule of thumb we use when advising buyers:
- Z0 (clearance) — only for single-axis applications where the load direction is constant and precision is not critical. Rarely the right choice for a machine tool.
- Z1 (light preload) — the default for most automation. Good stiffness, acceptable friction, long life. Start here unless you have a specific reason not to.
- Z2 (medium preload) — required when the machine experiences overturning moments or when positioning accuracy under varying load is critical. Common on CNC machines with two carriages per rail.
- Z3 (heavy preload) — only for rigid, low-duty-cycle machines. The life penalty is significant; verify the calculated life before committing.
One practical note: higher preload requires higher drive force. If you are retrofitting an existing machine, check that the servo or stepper motor has enough torque margin to overcome the increased friction of a heavier preload class.
3. Mounting Options and Accuracy Grades
The linear bearing block is only as good as the surfaces it mounts to. Accuracy grade and mounting surface finish are the two factors that determine whether the theoretical precision of the block is actually achieved on the machine.
Accuracy Grades
Manufacturers classify linear carriage assemblies into accuracy grades, typically C0 (highest) to C5 (standard), based on the parallelism of the running surface relative to the mounting surface, and the height tolerance of the block.
| Accuracy Grade | Height Tolerance (typical, per 100 mm) | Typical Applications |
|---|---|---|
| C0 / Ultra precision | ±3 µm | Semiconductor, precision measurement, high-end machining |
| C1 / High precision | ±5 µm | Precision CNC, EDM, grinding |
| C2 / Precision | ±7 µm | Standard CNC, laser cutting |
| C3 / Medium precision | ±10 µm | General automation, packaging |
| C5 / Standard | ±20 µm | Material handling, basic positioning |
Here is the key point: a C0 carriage mounted on a poorly machined surface performs worse than a C3 carriage on a properly machined surface. The mounting surface flatness should be within 1–2 µm per 100 mm for high-precision grades, and the mounting screws must be torqued to spec — uneven clamping distorts the rail and introduces binding.
Mounting Configurations
There are two common mounting arrangements for the linear guide bearing block:
- Flange type (low profile) — the block has flanges on both sides for mounting from above. Easier to install, more compact, but slightly lower load capacity for the same width.
- Square type (narrow) — mounting from below, with a narrower profile. Higher rigidity for the same width, but requires access to the underside of the block during installation.
For applications with heavy moment loads, consider using two carriages per rail. This doubles the load capacity and, more importantly, resists overturning moments far better than a single wider block. The trade-off is a longer assembly and more demanding alignment requirements.
4. Sealing, Lubrication, and Environmental Factors
Selection does not end with load and preload. The operating environment dictates the sealing and lubrication options:
- Standard seals (contact) — for clean, indoor environments. Low friction, adequate protection against fine dust.
- Double seals — for machining environments with coolant, chips, or abrasive dust. Higher friction, but significantly longer life in dirty conditions.
- Scraper plates (metal or plastic) — for welding, grinding, or woodworking where large debris is present. These scrape off particles before they reach the seals.
- Lubrication — factory grease (lithium-based, NLGI 2 is common) is standard. For high-speed or food-grade applications, specify the appropriate grease type. Consider a central lubrication system for machines with many carriages or hard-to-reach positions.
If the machine operates in a temperature range outside 0–40°C, confirm with the supplier that the seals and grease are rated for the actual conditions. Standard seals harden at low temperatures and degrade above 80°C.
5. Supplier Evaluation Checklist
When comparing quotes from different suppliers, make sure you are comparing the same specification. Use this checklist:
| Item | What to Verify | Why It Matters |
|---|---|---|
| Dynamic load rating (C) | Value in N or kN, and the travel basis (usually 50 km) | Determines calculated service life |
| Static load rating (C0) | Value in N or kN | Determines static safety factor |
| Preload class | Exact symbol and definition | Different manufacturers use different symbols |
| Accuracy grade | C0–C5, with height tolerance values | Determines achievable positioning precision |
| Rail straightness | µm per meter | Affects smoothness and noise |
| Material and hardness | Bearing steel grade, hardness HRC | Affects wear life and load capacity |
| Seal configuration | Standard, double, or scraper | Matches the operating environment |
| Dimensional report | Certified measurement data per batch | Verifies the block meets spec before installation |
| Material certificate | Mill test certificate for the steel | Traceability for quality control |
If a supplier cannot provide a dimensional report or material certificate, ask why. For precision motion components, these documents are standard practice — not a special request.
Frequently Asked Questions
What is the difference between a linear carriage and a linear bearing block?
They refer to the same component. Linear carriage and linear guide bearing block are interchangeable terms for the moving block that rides on a linear guide rail. Some catalogs use "carriage" for the block-and-rail assembly and "bearing block" for the block alone, but in practice the terms overlap.
How do I know if I need a wider rail or a second carriage?
If the limiting factor is moment load (overturning force), a second carriage on the same rail is usually more effective than a wider single block. If the limiting factor is vertical load capacity, a wider block is the simpler solution. Calculate both loads separately before deciding.
Can I mix carriages from different manufacturers on the same rail?
Not recommended. Rail profile, ball diameter, and preload geometry are manufacturer-specific. Mixing brands can cause uneven load distribution, premature wear, and binding. If you are replacing a single linear guide bearing block in an existing system, match the original brand and part number, or replace the entire rail-and-block assembly.
How often should a linear carriage be lubricated?
For standard factory grease, re-lubricate every 100–200 km of travel, or every 3–6 months in normal duty. Machines with coolant exposure or abrasive dust need more frequent lubrication. Many manufacturers offer centralized lubrication ports on the block — specify these if the carriage is hard to reach.
Final Recommendation
Start your selection with the load spectrum, not the catalog. Calculate the equivalent dynamic load, apply the static safety factor for your application type, then choose the preload class that matches your stiffness requirements. Verify the accuracy grade against your positioning tolerance, and confirm the mounting surface finish is adequate for that grade.
When you send an inquiry to a supplier, include the following: rail width, block type (flange or square), preload class, accuracy grade, seal type, and the load values you calculated. A supplier that responds with a recommendation — not just a quote — is one that understands the application. Ask for the dimensional report and material certificate before placing the order, not after.
If you are sourcing linear carriages for a new machine or a retrofit, and you want a second opinion on your load calculations or preload selection, send us your application details. We can review the numbers and recommend a configuration that balances life, cost, and performance.