Heavy Duty Linear Guide: High-Load Guideway Solutions
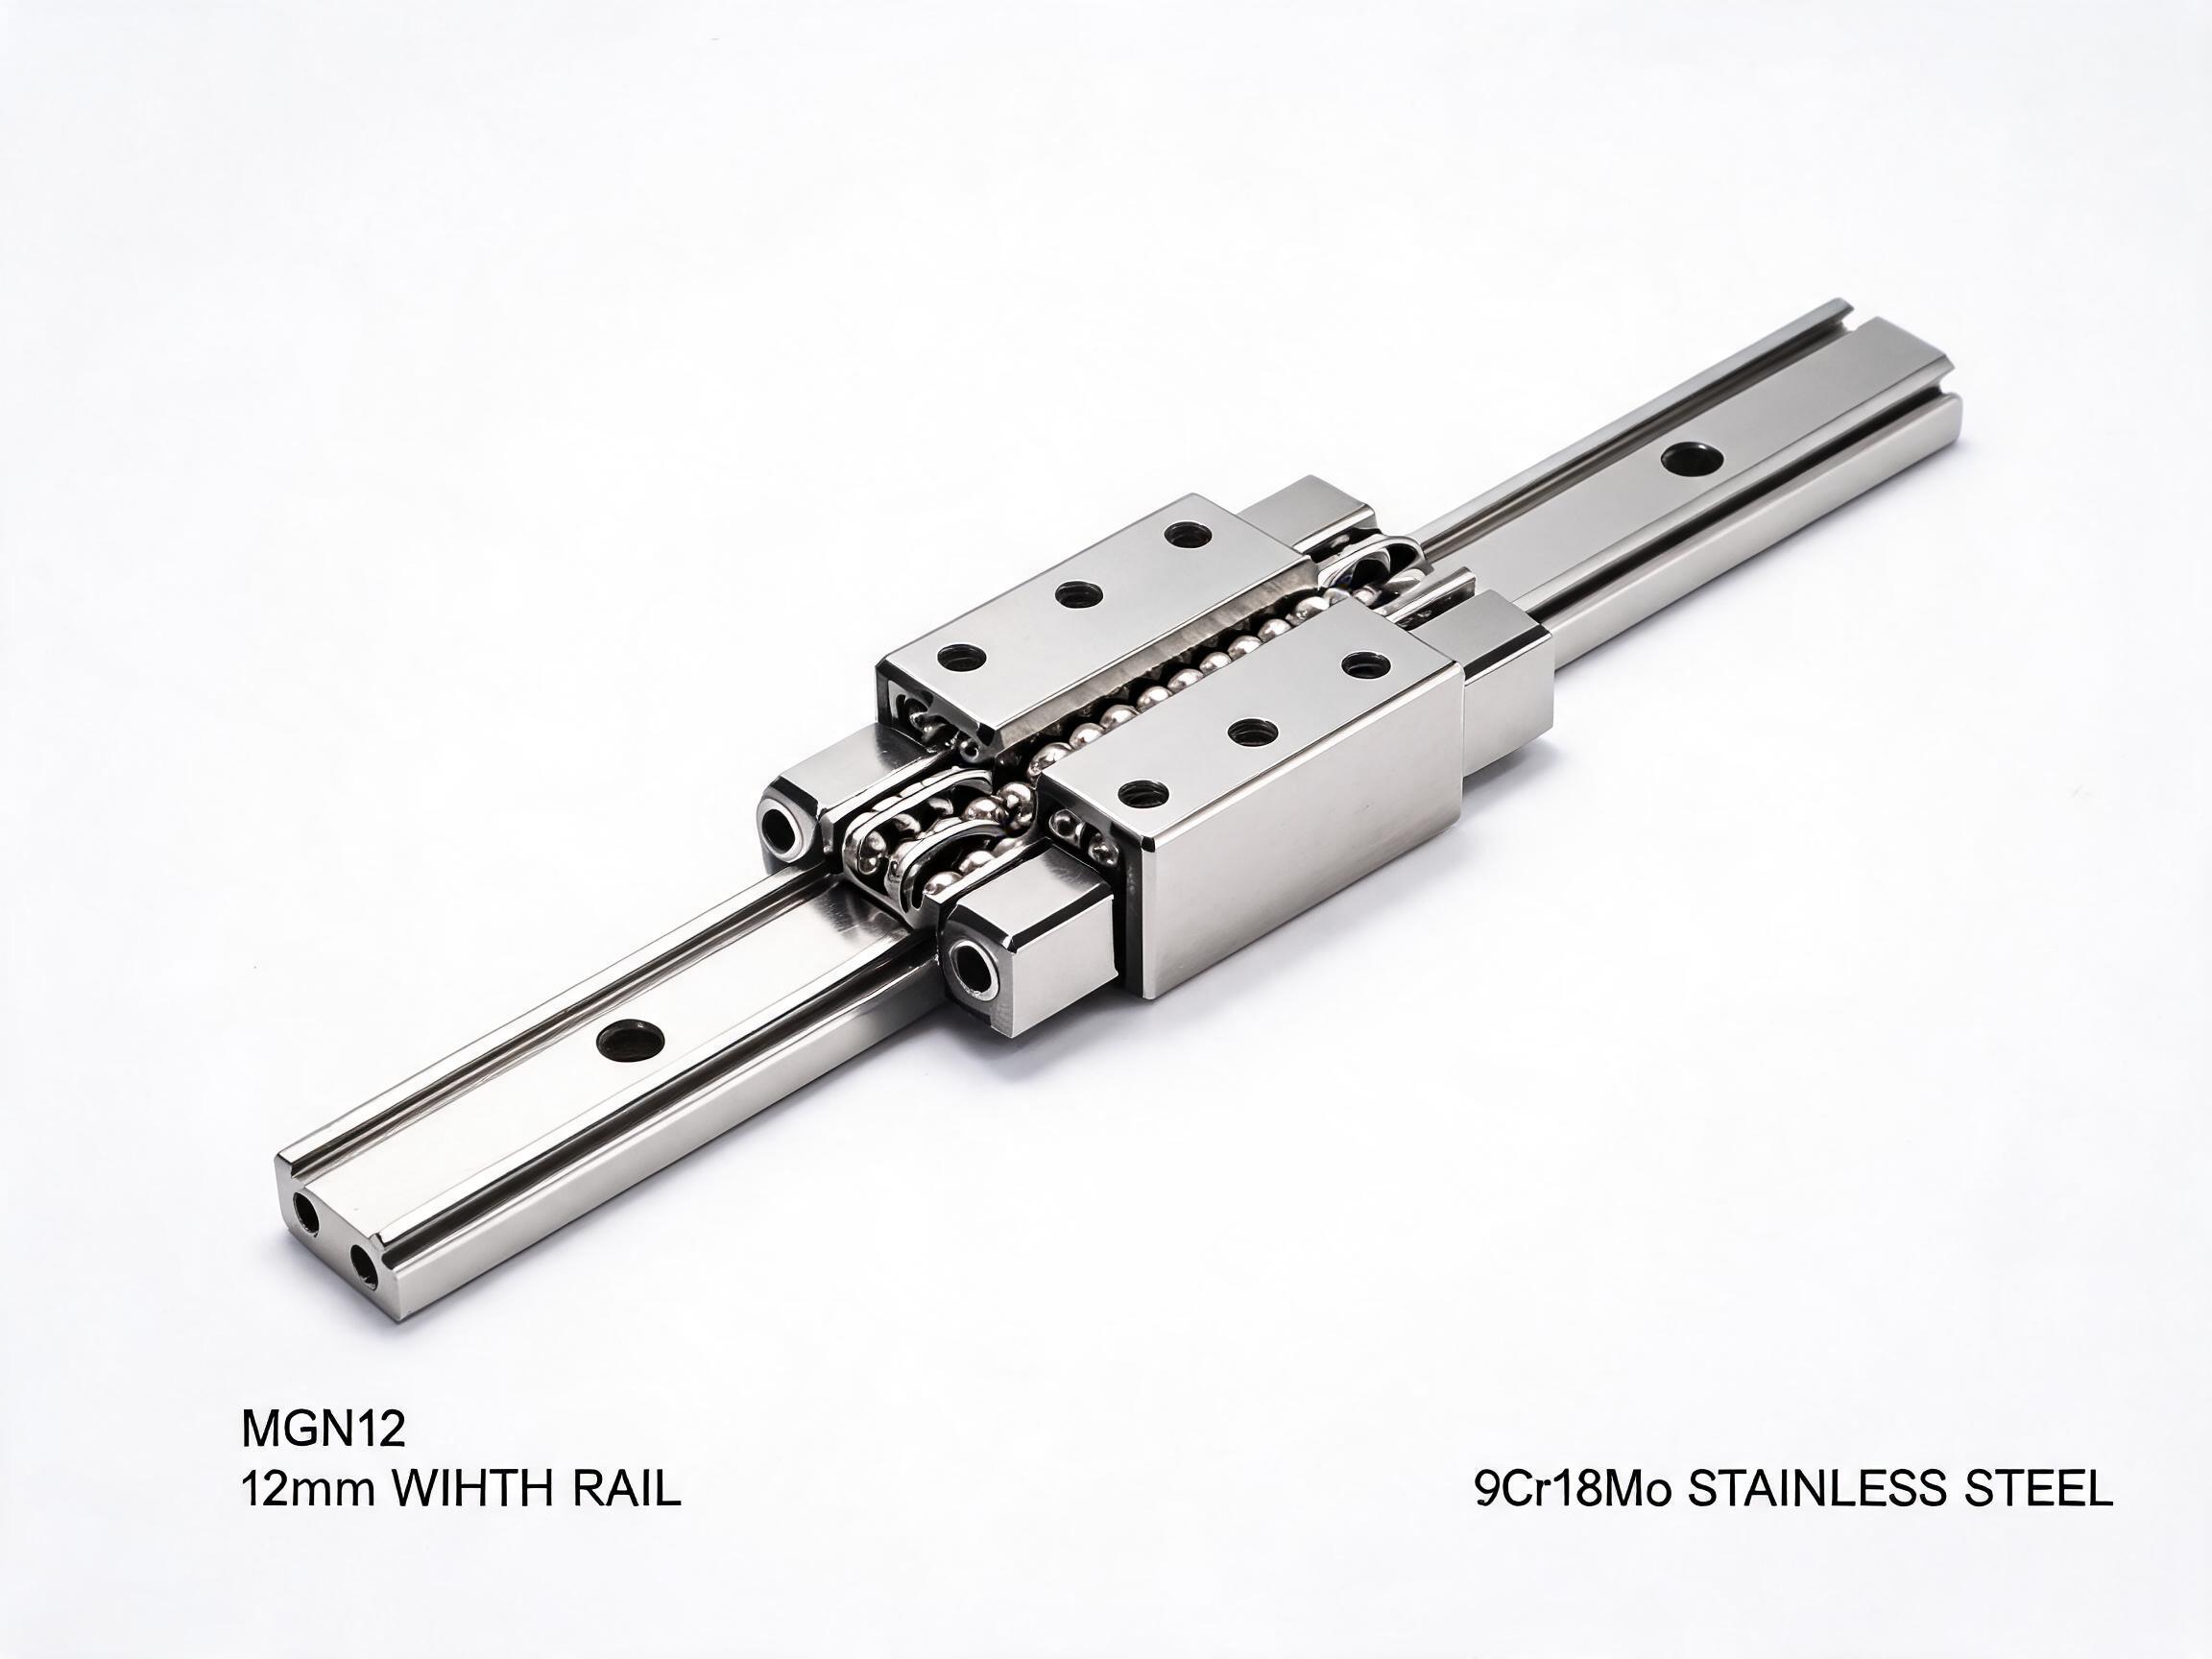
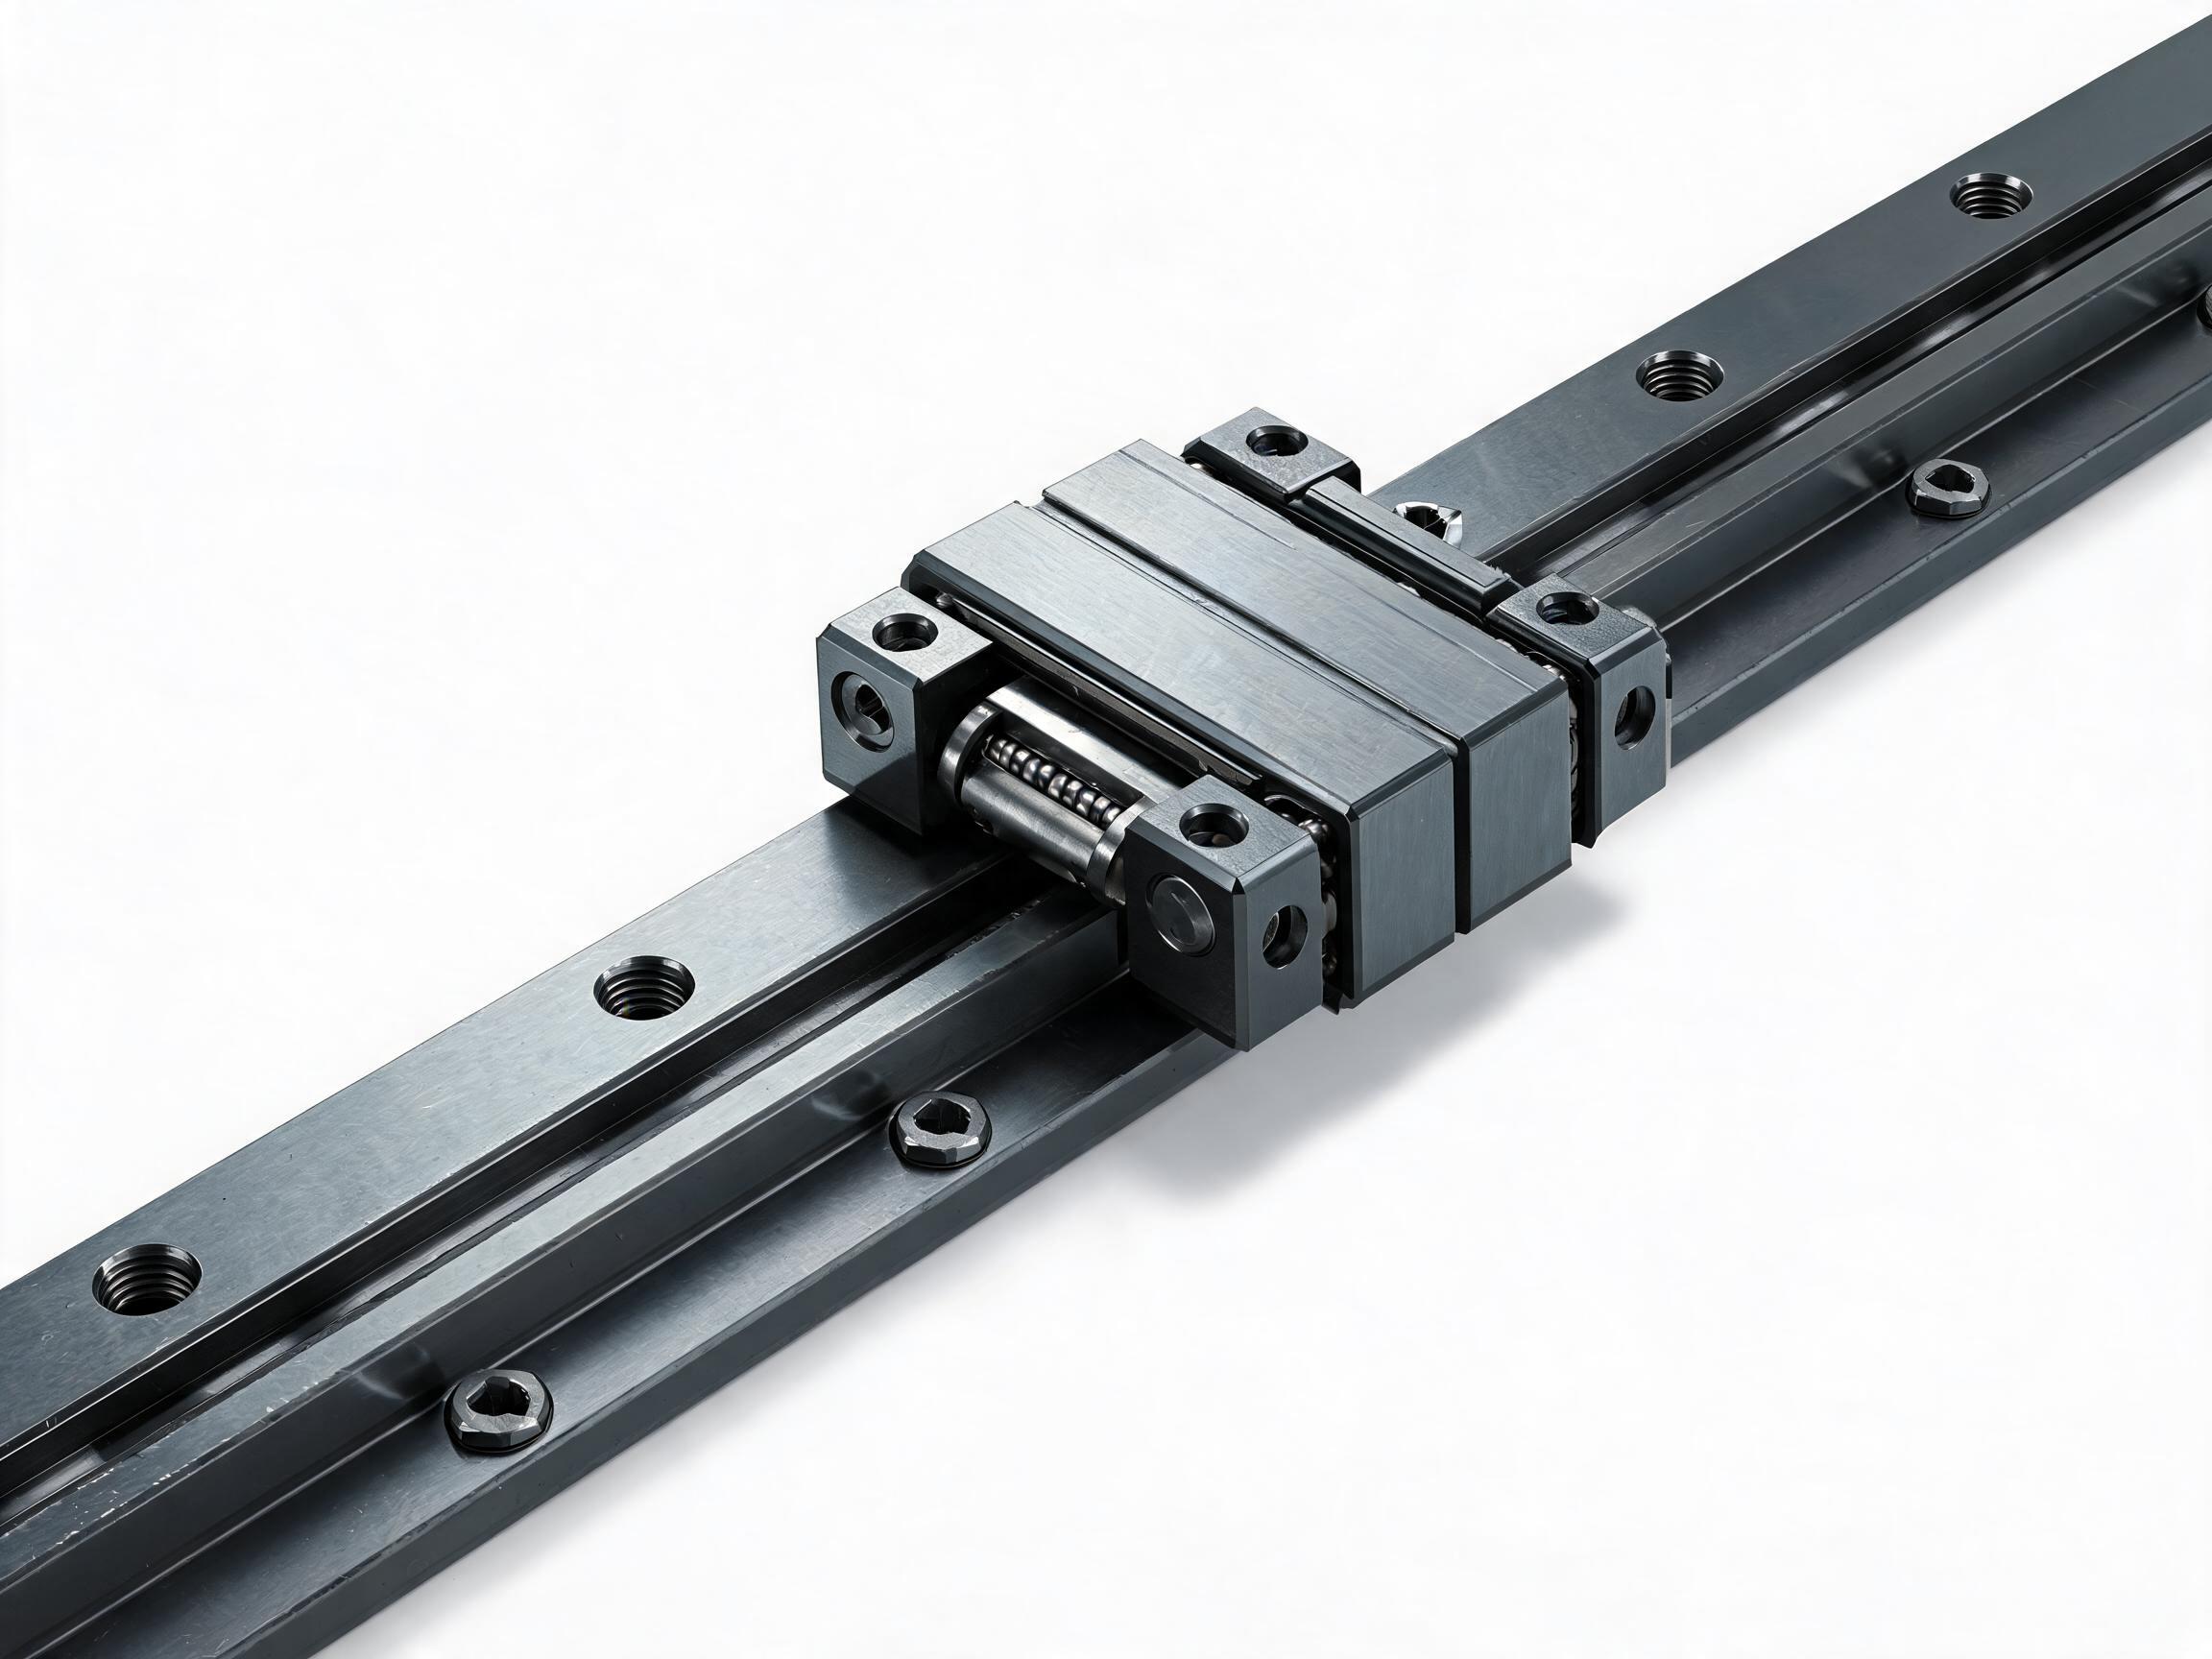
A heavy duty linear guide is a guideway system engineered for applications where dynamic loads exceed 30 kN, requiring larger rail cross-sections, higher carriage load capacity, and specialized preload configurations to maintain precision under extreme forces. Dongfeng Bearing manufactures the HGR35 and HGR45 heavy duty guide rails specifically for injection molding machines, press equipment, heavy CNC machining centers, stamping dies, and large automation structures where standard 15-25 mm rails are insufficient. The HGR45, the largest in the series, provides 84.5 kN dynamic load and 168 kN static load capacity, with rail widths of 45 mm and standard lengths up to 4000 mm.
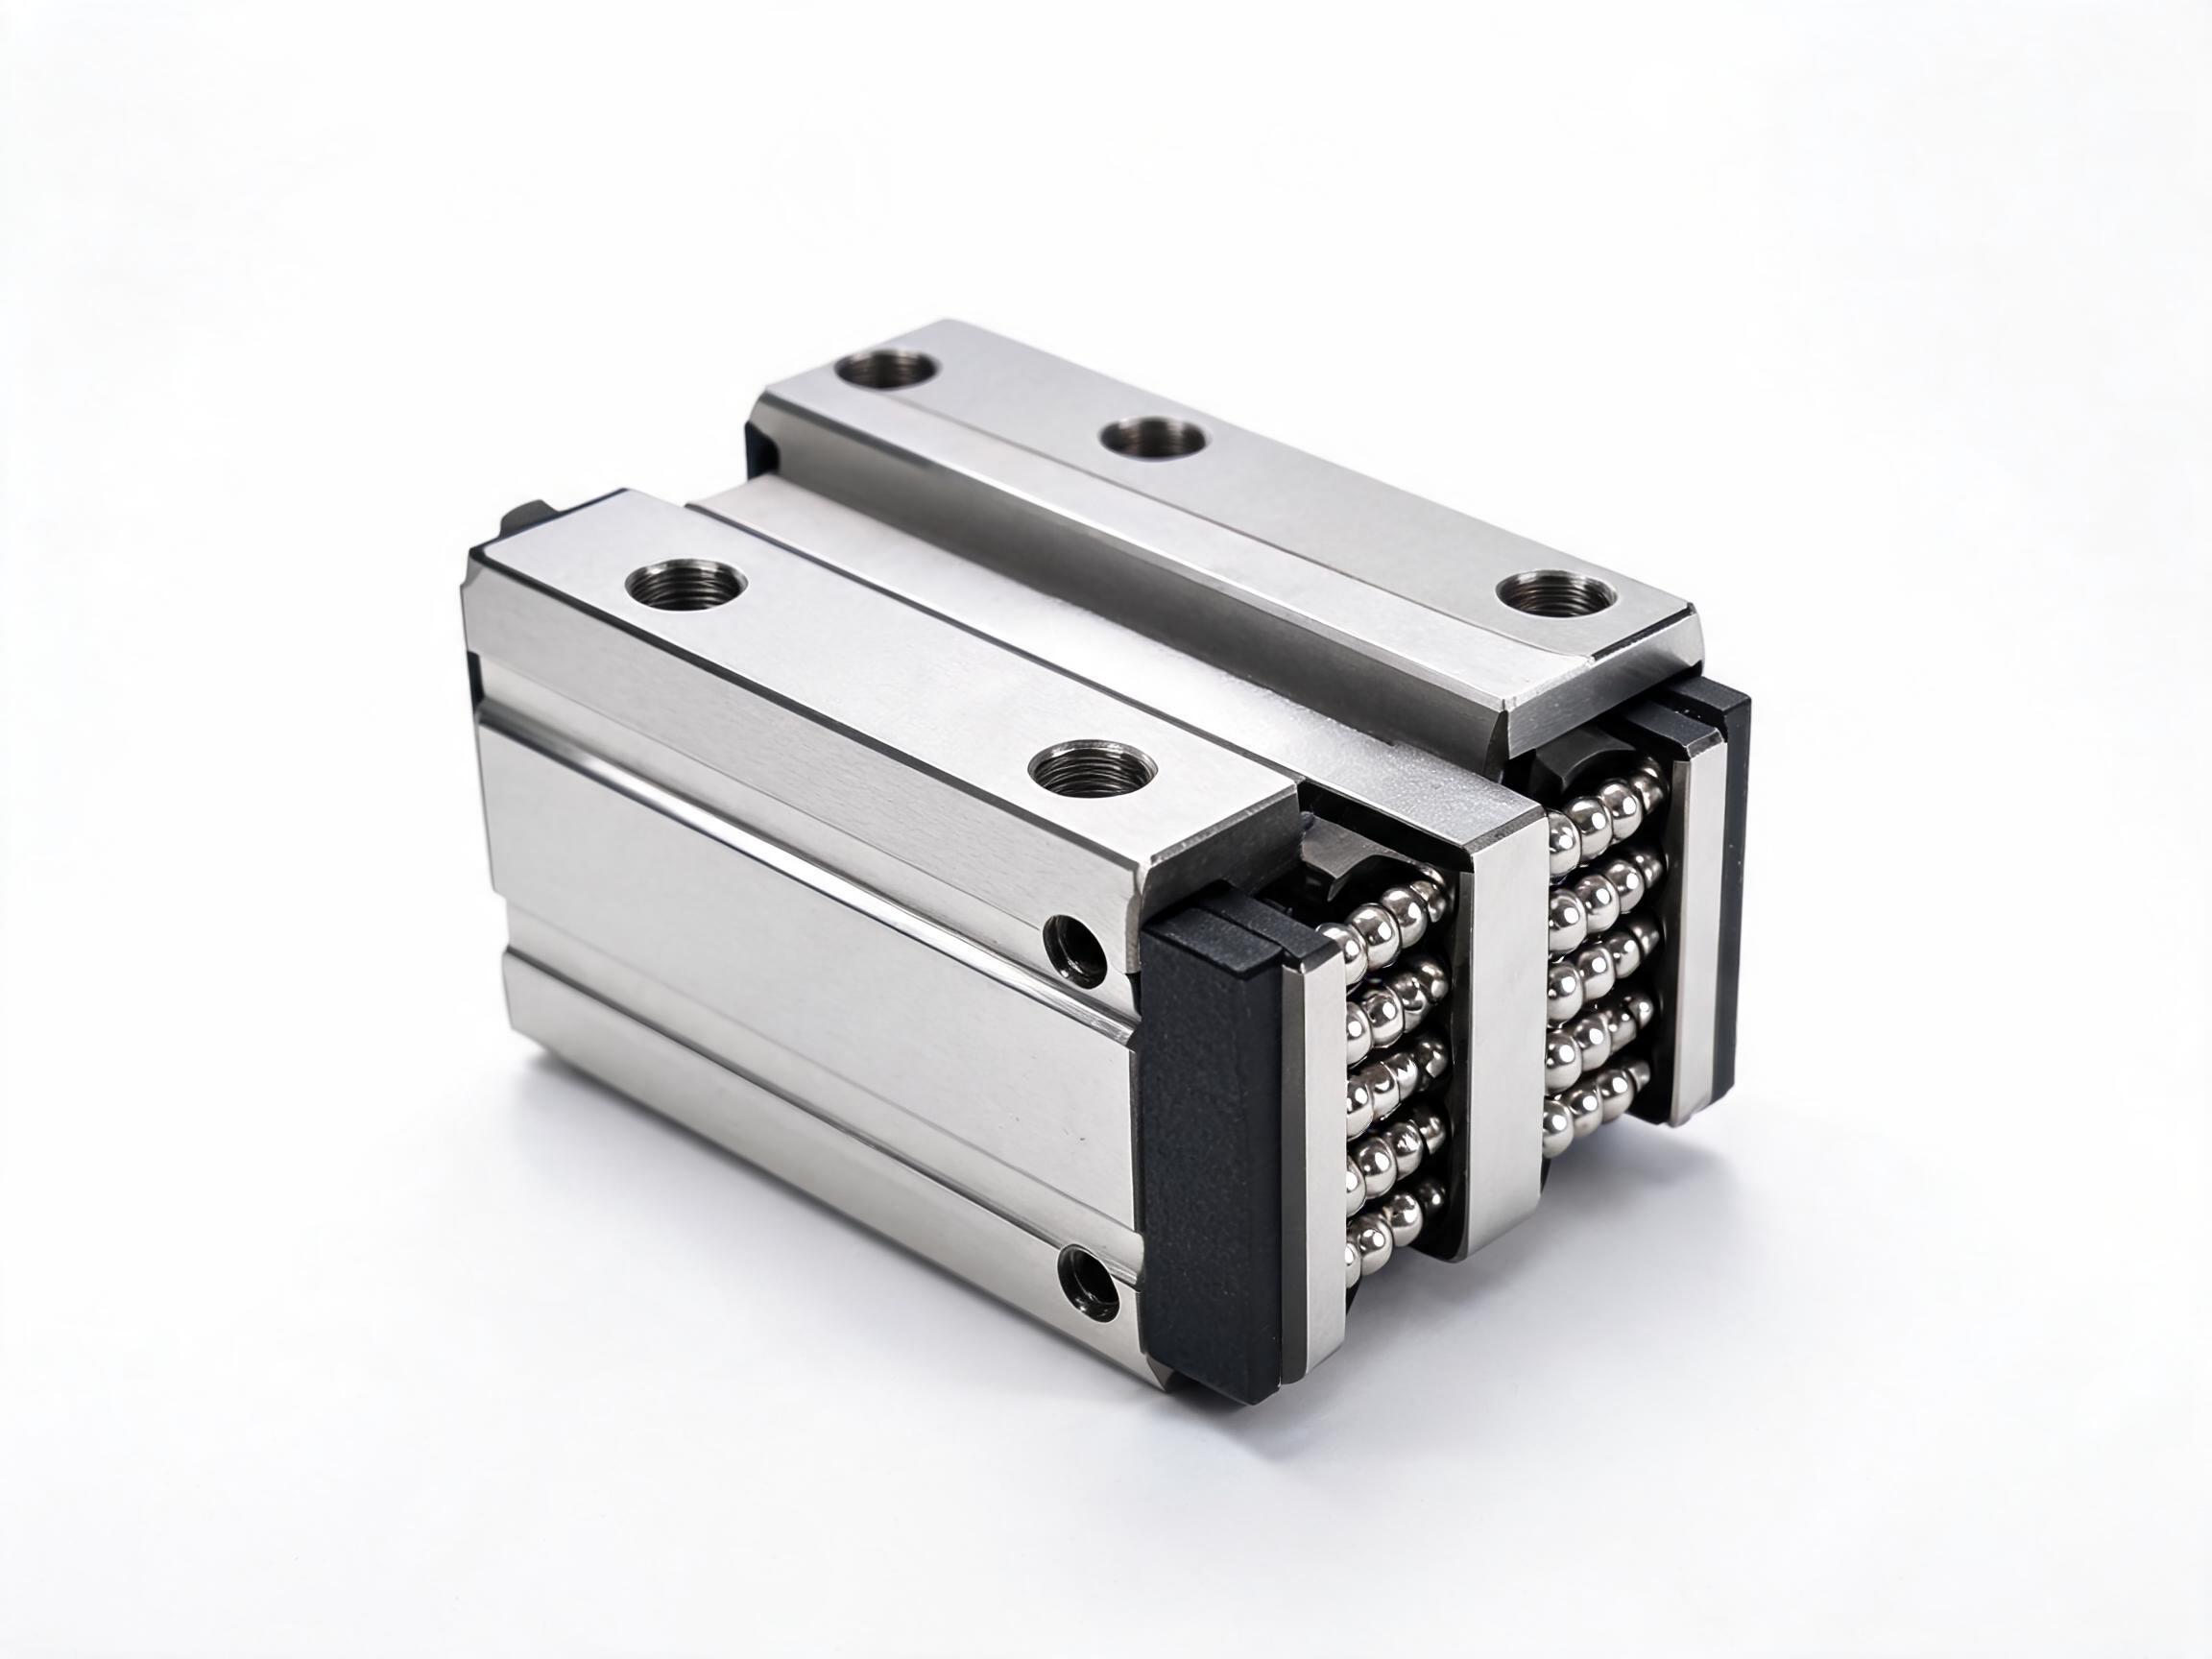
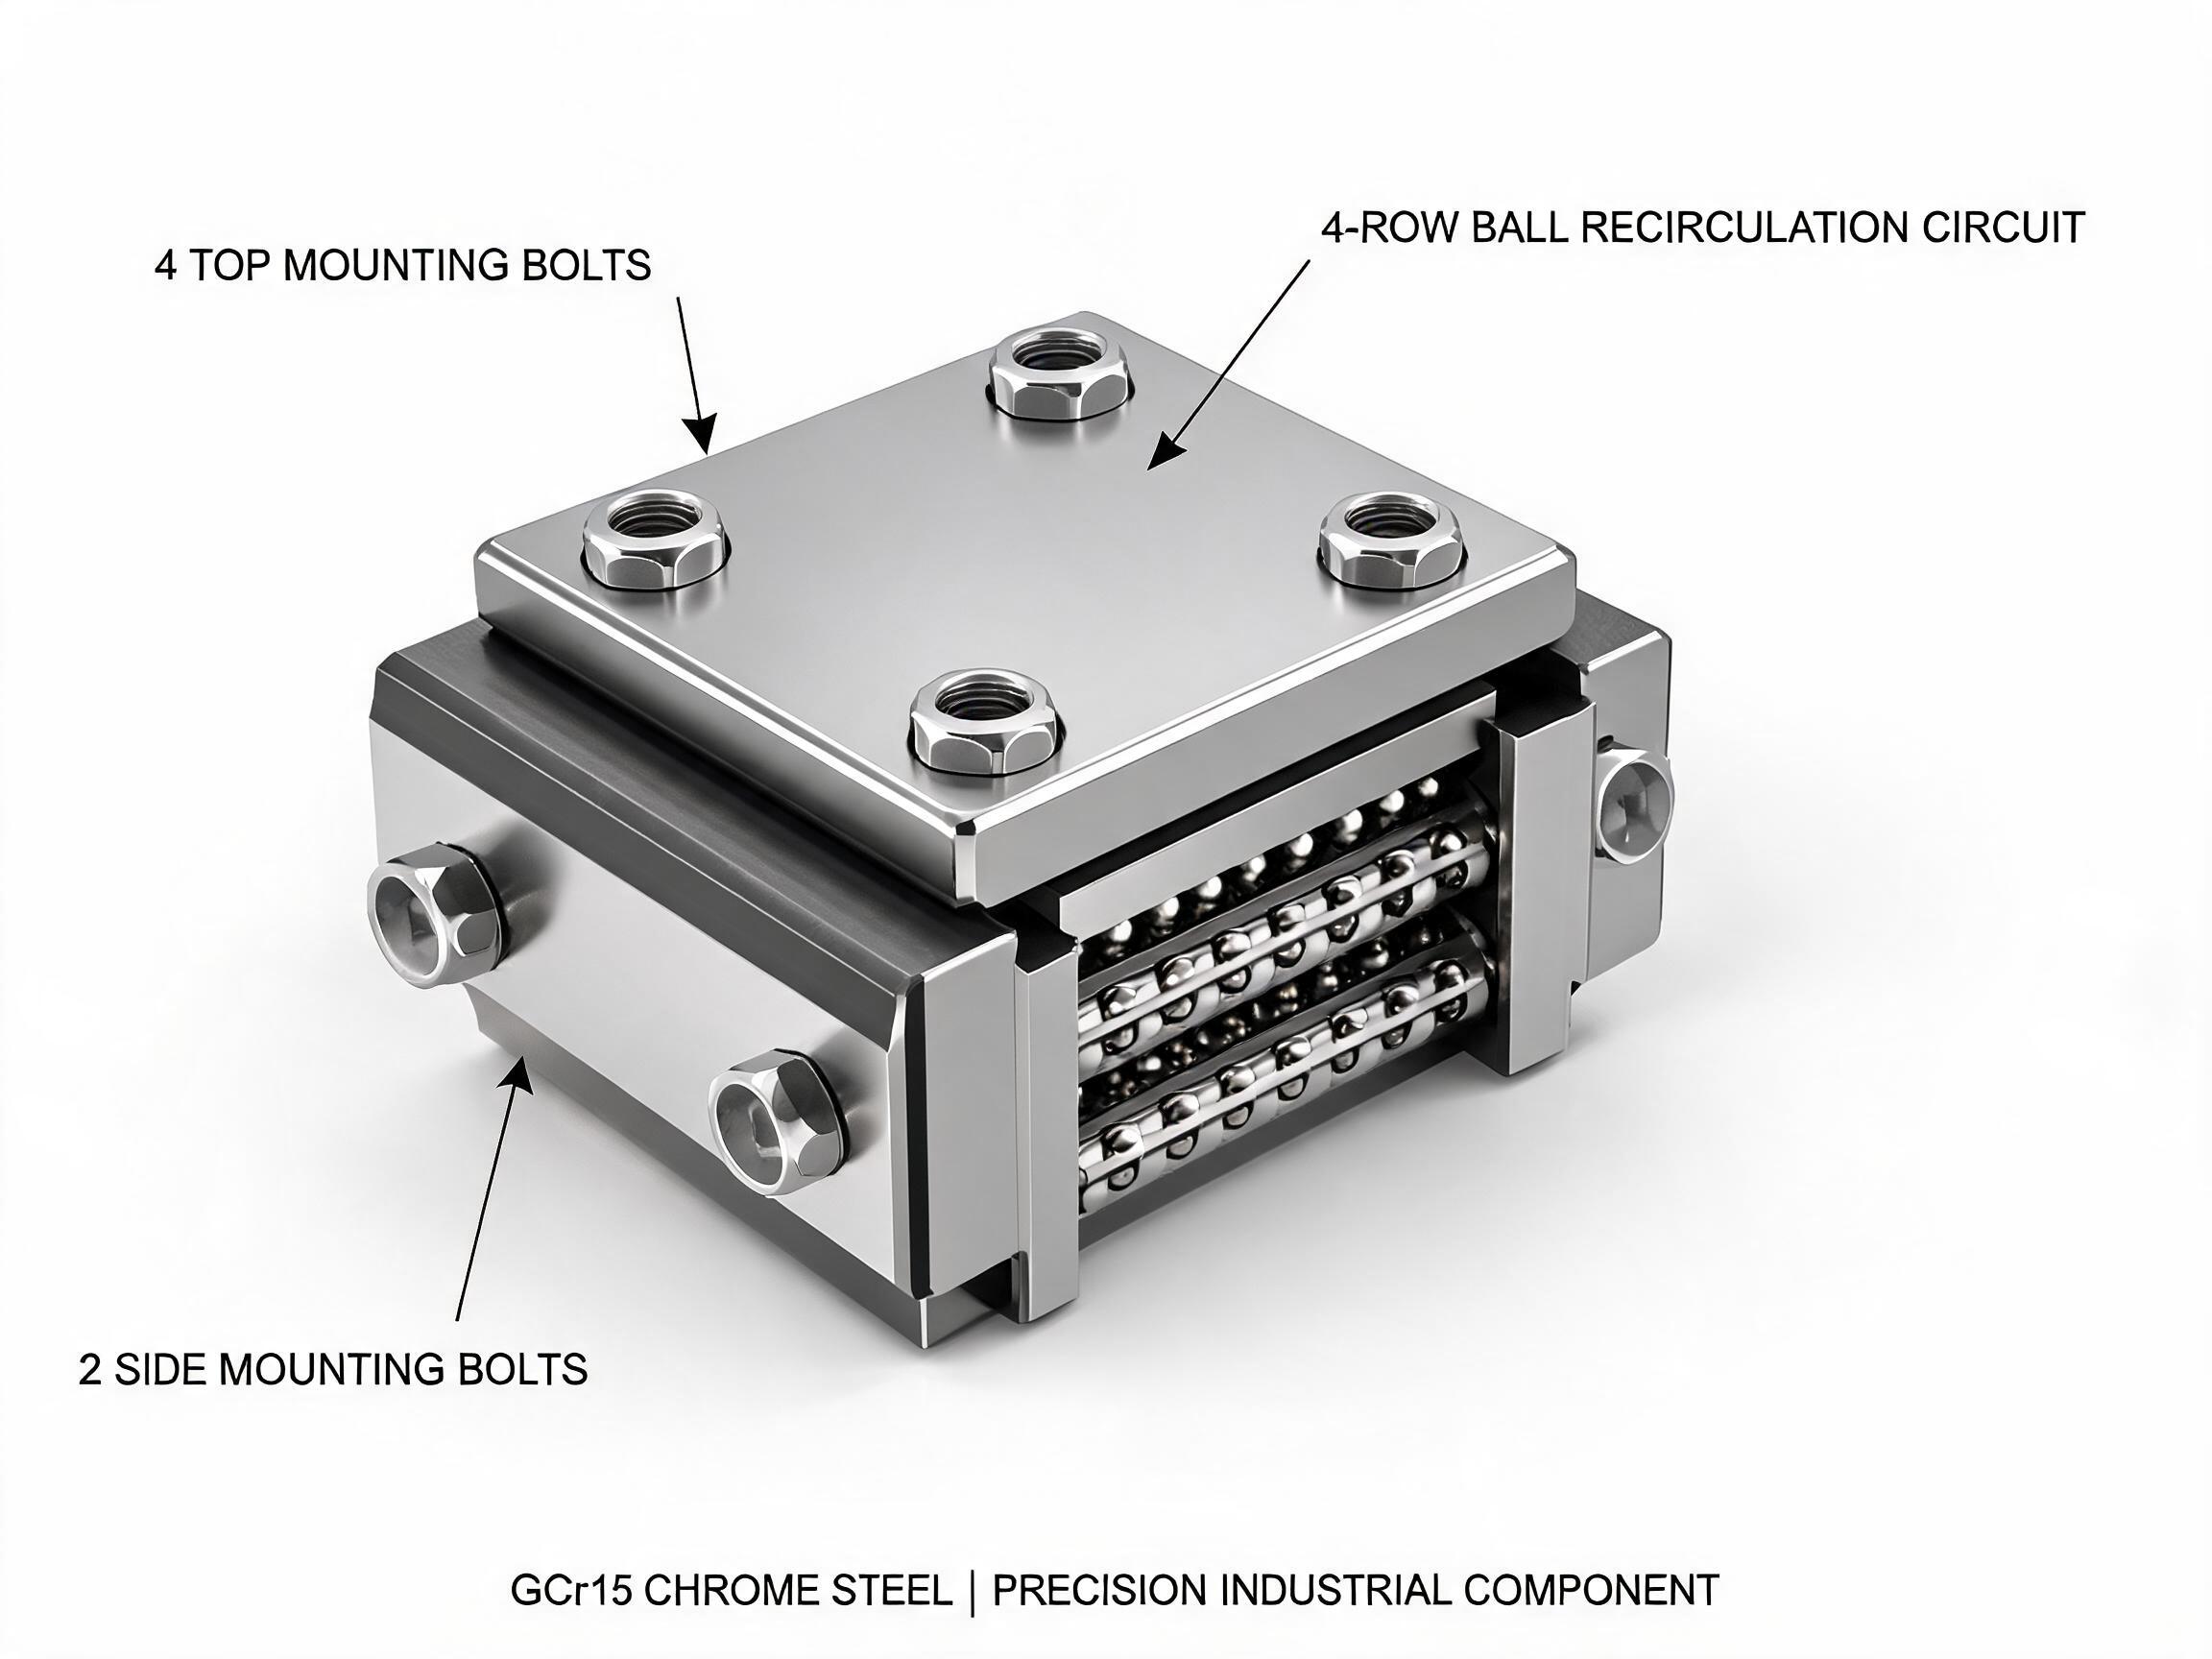
Heavy duty guide rails differ from standard sizes in several engineering aspects beyond dimensional scaling. The rail cross-section is proportionally thicker to resist bending under high point loads. Carriage blocks contain larger ball diameters with more balls per circuit, distributing Hertzian contact stresses over a wider area. The four-row geometry becomes critical at these loads, as any asymmetry in ball loading causes uneven wear and premature failure. HGR35 and HGR45 carriages use reinforced end caps and thicker seal carriers to withstand the higher forces and longer lever arms encountered in heavy machinery.
| Heavy Duty Rail | Width | Dynamic Load | Static Load | Carriage Options | Max Length |
|---|---|---|---|---|---|
| HGR35 | 35 mm | 52.6 kN | 78.4 kN | HGH35, HGW35 | 4000 mm |
| HGR45 | 45 mm | 84.5 kN | 168 kN | HGH45, HGW45 | 4000 mm |
Applications Requiring Heavy Duty Linear Guides
Injection molding machines with 200-500 ton clamping force generate guide loads of 20-60 kN per rail during mold open and close cycles, requiring HGR35 or HGR45 rails with ZC heavy preload. CNC machining centers for heavy steel milling with 30 kW or larger spindles produce cutting forces above 5000 N, needing HGR35 rails for adequate travel life. Stamping presses with 100-300 ton capacity use HGR45 rails for die guidance with continuous loads of 50-100 kN. Large gantry milling machines for aerospace components require HGR45 on the X-axis with travel lengths of 3000-4000 mm. Automotive welding stations with robotic arms and heavy fixtures use HGR35 rails for positioning accuracy under high static and dynamic loads.
HGR45 Specifications and Performance Data
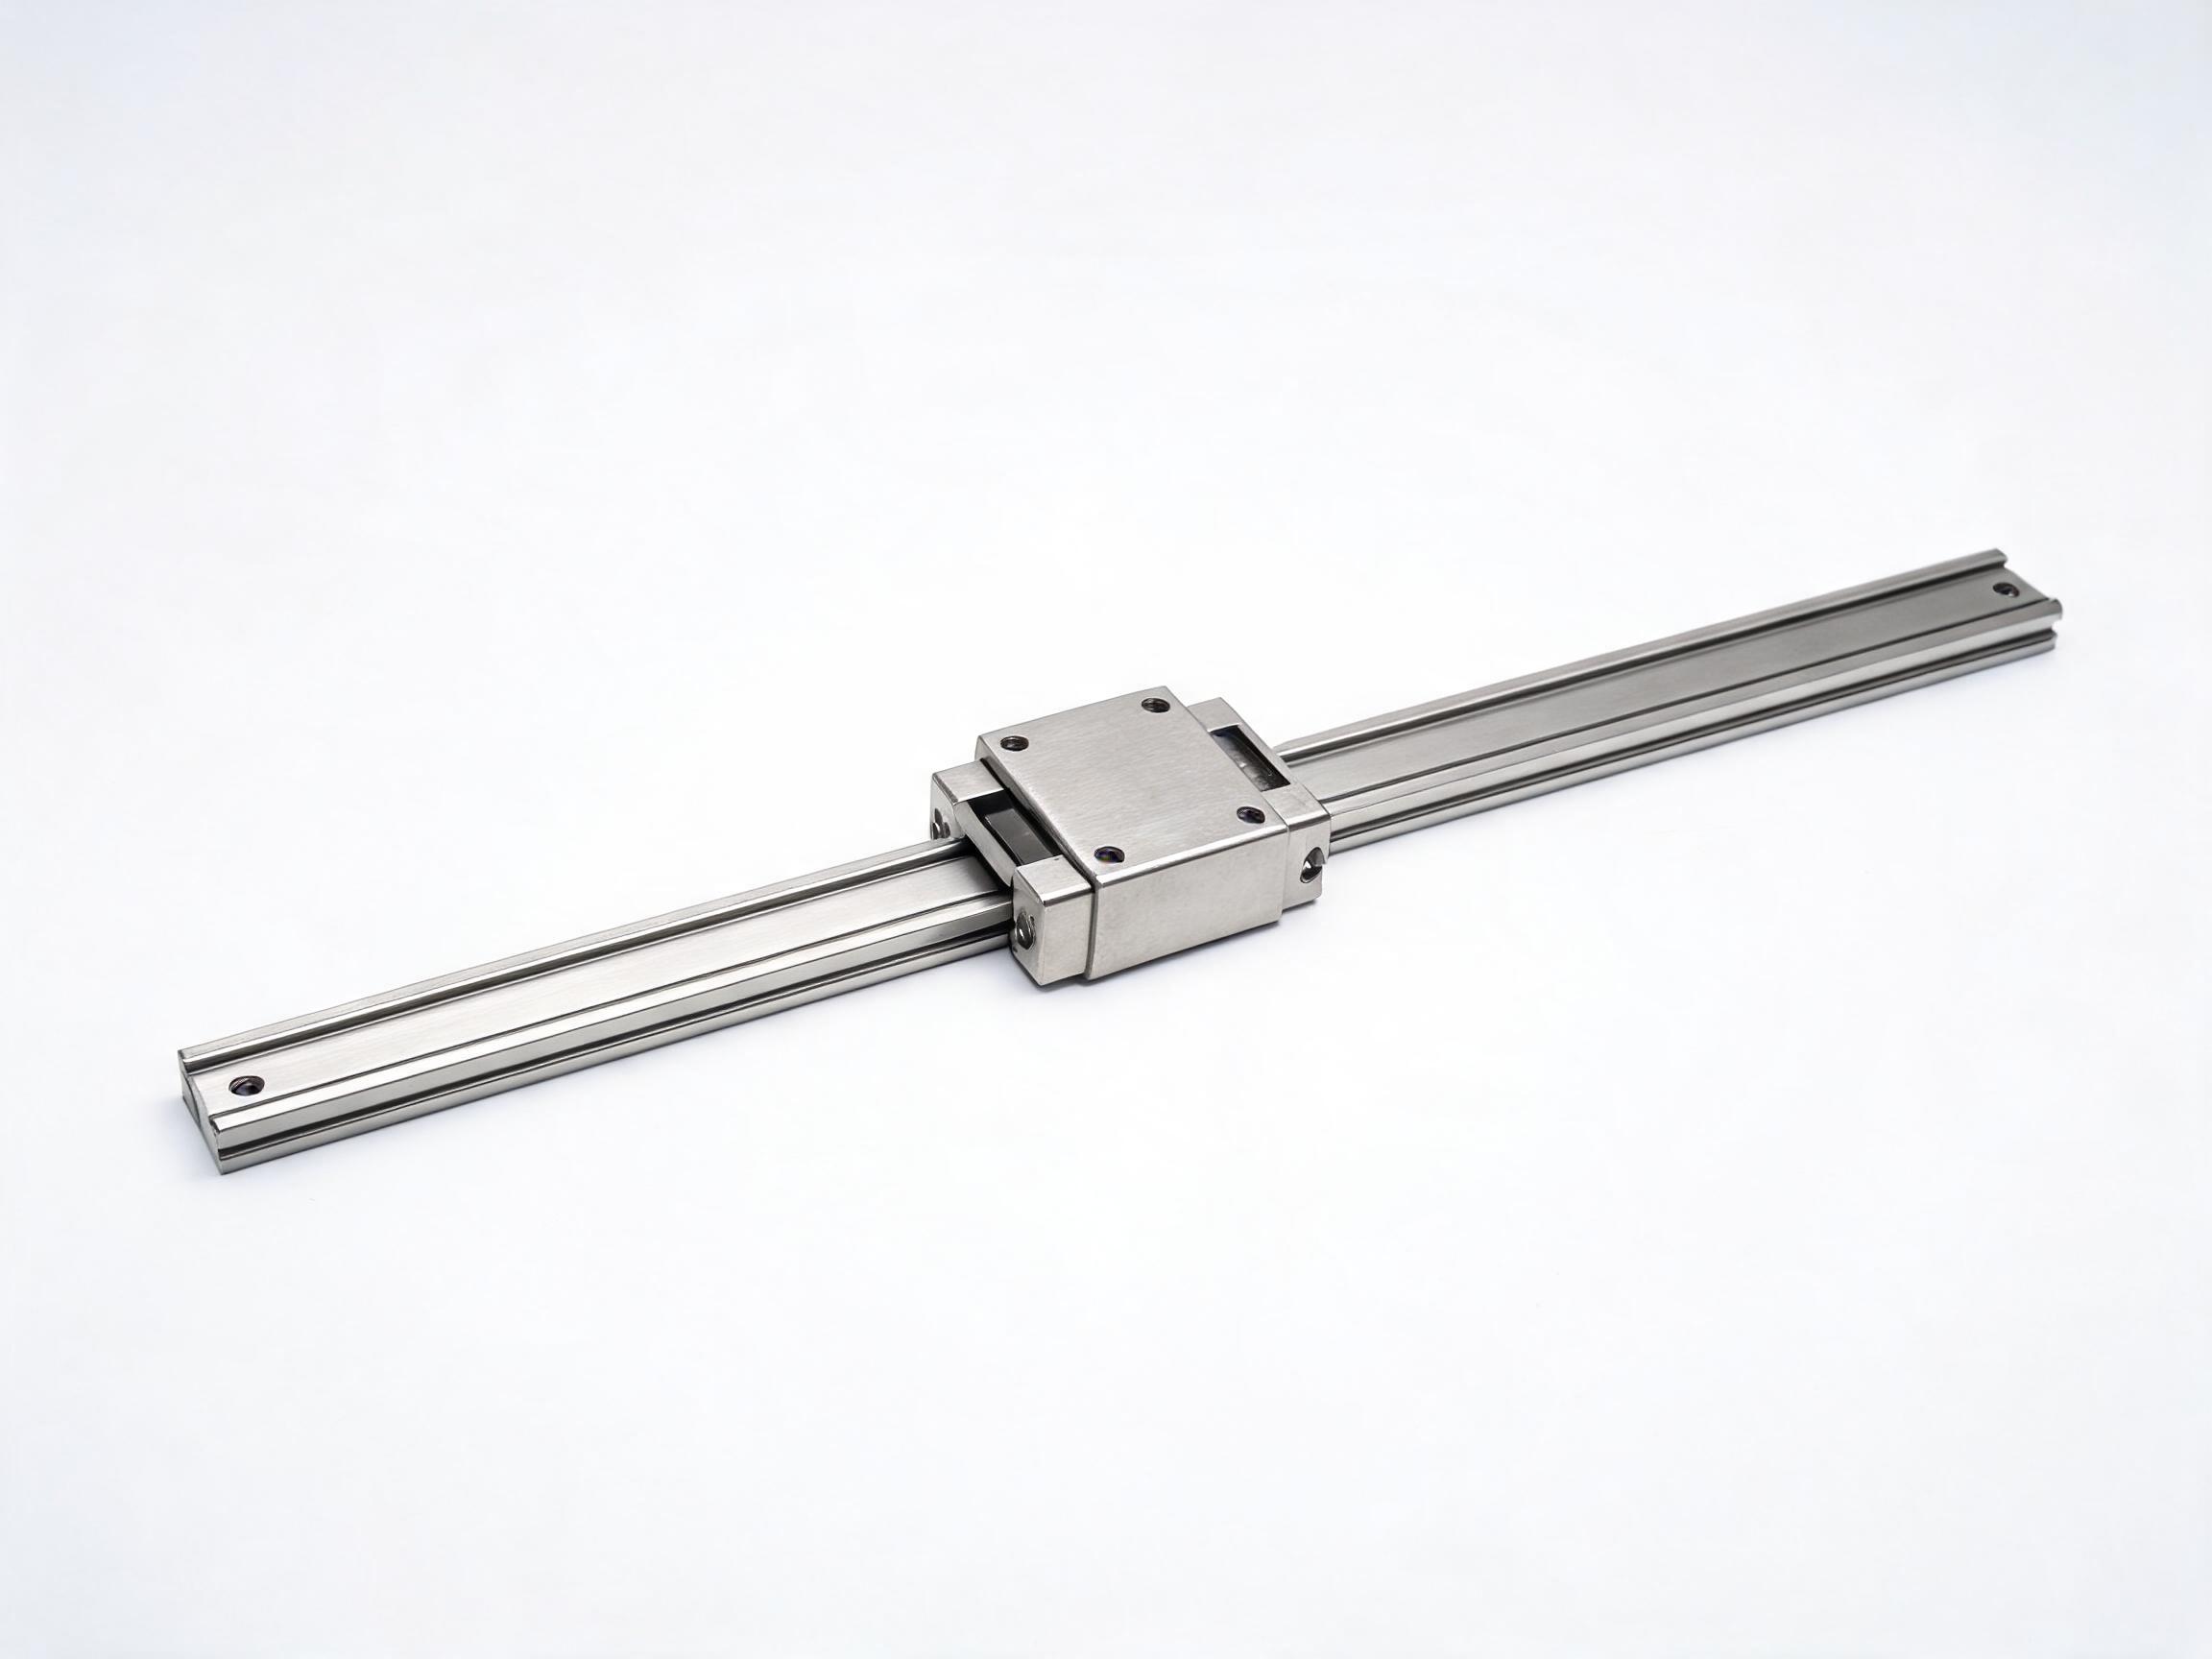
The HGR45 rail features a 45 mm width, 60 mm height, and standard lengths from 1000 to 4000 mm. The HGH45 flange carriage provides 84.5 kN dynamic load and 145 kN static load with a 122 mm carriage length. The HGW45 wide-body carriage increases static load to 168 kN with a 134 mm length. Both use 9.525 mm diameter balls in four circuits with 15 balls per loading zone. Rail weight is 8.4 kg per meter. Mounting bolts are M16 grade 12.9, torqued to 180 Nm. The rail shoulder height is 7 mm for positive lateral location.
| Parameter | HGR45 + HGH45 | HGR45 + HGW45 |
|---|---|---|
| Dynamic load (C) | 84.5 kN | 84.5 kN |
| Static load (C0) | 145 kN | 168 kN |
| Carriage length | 122 mm | 134 mm |
| Ball diameter | 9.525 mm | 9.525 mm |
| Mounting | Top or bottom | Top only |
| Weight per meter | 8.4 kg | 8.4 kg |
Preload and Rigidity for Heavy Load Applications
For heavy duty applications, ZC (heavy preload, 0.10C to 0.12C) is typically selected to eliminate clearance under high loads. For HGR45 with ZC preload, the preload force is 8.5-10.1 kN, providing radial rigidity of approximately 950 N per micrometer. This rigidity limits carriage deflection to less than 5 microns under full dynamic load, essential for maintaining injection molding precision or machining accuracy. However, ZC preload reduces travel life by approximately 30 percent compared to ZB; for applications requiring both heavy load and long life, consider oversizing the rail by one size and using ZB preload instead.
Travel Life Calculation for Heavy Duty Guides
For injection molding machines operating at 30 kN load per carriage with HGR45 (C equals 84.5 kN), L10 equals 100 times (84.5 divided by 30) cubed equals 2,235 km. At 100 cycles per hour with 500 mm travel per cycle, annual travel is 100 times 500 times 2 times 6000 equals 600 km per year, yielding approximately 3.7 years L10 life. For a stamping press at 60 kN load, L10 equals 100 times (84.5 divided by 60) cubed equals 280 km, or about 6 months at 600 km per year, requiring HGR45 with HGW carriages (168 kN static) or dual-rail configurations to distribute load.
Mounting and Foundation Requirements
Heavy duty guide rails require reinforced mounting surfaces rated for the applied loads. For HGR45 at 60 kN load, the mounting surface must withstand point loads of 15 kN per bolt without deflection exceeding 0.01 mm. Foundation steel thickness should be at least 25 mm for HGR35 and 35 mm for HGR45, with support ribs spaced at 200-300 mm intervals. Mounting bolt torque for HGR45 is 180 Nm using M16 grade 12.9 bolts. Reference shoulder height is 7 mm with shoulder contact width of at least 15 mm for lateral force transmission.
Multi-Rail Configurations for Load Distribution
When single-rail capacity is insufficient, dual-rail configurations distribute loads across twice the carriage area. For a 120 kN total load, two HGR45 rails with HGW45 carriages provide 338 kN combined static load capacity. In dual-rail setups, ensure equal load sharing by machining both mounting surfaces in a single setup, maintaining rail-to-rail parallelism within 0.02 mm per 300 mm. Use carriages of the same accuracy grade and preload class on both rails. For very high loads, consider four carriages per rail (two per rail per side) to further distribute loading.
Lubrication and Maintenance for Heavy Duty Guides
Heavy duty guides operating at high loads require more frequent lubrication than standard applications. Relubricate HGR35 and HGR45 carriages every 250-500 hours or 50 km of travel using lithium complex grease NLGI 2 with extreme pressure additives. For injection molding machines with automatic grease systems, set delivery rate to 0.5-1.0 grams per week per carriage. Monitor grease condition for metal particles indicating wear. Replace seals every 5000 hours in heavy load applications. Schedule annual CMM inspection of rail parallelism and carriage height to detect foundation settling or wear trends.
Quality Control for Heavy Duty Applications
For heavy duty guide rails, extended quality control includes ultrasonic testing of rail internal structure to detect forging defects, magnetic particle inspection of raceway surfaces, and 100 percent hardness testing (not batch sampling) on HGR45 rails. CMM inspection covers parallelism at five points along the rail, with maximum deviation limited to 80 percent of grade tolerance. Carriage load testing verifies actual dynamic load capacity before shipment. SGS material certificates confirm steel composition, and CE conformity documentation supports heavy machinery compliance requirements.
OEM Engineering Support for Heavy Machinery
Dongfeng Bearing provides OEM engineering support for heavy machinery manufacturers including custom rail lengths up to 4000 mm, special preload classes for specific load profiles, matched carriage sets with height variation within plus-minus 0.005 mm, custom seal designs for harsh environments, and modified mounting configurations for existing machine retrofits. Engineering support includes load calculation, rail selection, and mounting design review. Lead time for HGR45 standard sizes is 25-35 working days; custom configurations require 30-40 working days.
Frequently Asked Questions
What loads require a heavy duty linear guide?
Applications with dynamic loads above 30 kN per carriage should use HGR35 (52.6 kN) or HGR45 (84.5 kN). Standard HGR20 and HGR25 rails are rated for 14.7 kN and 22.4 kN respectively, insufficient for heavy machinery.
What is the maximum load capacity of HGR45?
HGR45 with HGH45 carriage: 84.5 kN dynamic, 145 kN static. With HGW45 wide-body carriage: 84.5 kN dynamic, 168 kN static. For higher loads, use dual-rail configurations to distribute loading.
What preload is recommended for injection molding machines?
ZC (heavy preload, 0.10C to 0.12C) for injection molding to eliminate clearance during clamping. For HGR45, preload force is 8.5-10.1 kN, providing approximately 950 N per micrometer radial rigidity.
How long do heavy duty guide rails last?
At 30 kN load, HGR45 L10 life is 2,235 km (approximately 3.7 years in injection molding). At 60 kN, L10 drops to 280 km. Heavy loads reduce life exponentially; oversizing the rail by one size can double or triple travel life.
What mounting surface is required for HGR45?
Foundation steel thickness at least 35 mm with support ribs every 200-300 mm. M16 grade 12.9 bolts torqued to 180 Nm. Reference shoulder height 7 mm with 15 mm contact width. Surface flatness 0.02 mm per 300 mm.
Can I use dual rails to increase load capacity?
Yes. Two HGR45 rails with HGW45 carriages provide 338 kN combined static capacity. Maintain rail-to-rail parallelism within 0.02 mm per 300 mm and use identical accuracy grades and preload classes on both rails.
How often should heavy duty guides be lubricated?
Every 250-500 hours or 50 km of travel using lithium complex grease NLGI 2 with EP additives. For automatic grease systems in injection molding, set delivery to 0.5-1.0 grams per week per carriage.
What quality inspections are performed on HGR45 rails?
Ultrasonic internal structure testing, magnetic particle inspection, 100 percent hardness testing (not batch sampling), CMM parallelism at five points, and carriage load testing. SGS material certificates and CE conformity included.
Are HGR45 rails available in custom lengths?
Yes, up to 4000 mm. Standard lead time 25-35 working days. Custom configurations with special preload, matched carriage sets, and modified mounting require 30-40 working days.
What is the cost comparison between HGR35 and HGR45?
HGR45 costs approximately 40-60 percent more than HGR35 due to larger material volume and longer machining cycles. The upgrade doubles static load capacity (78.4 to 168 kN), justified for applications above 50 kN dynamic load.